Choosing the best Pvc Profile Mixer in 2026 requires more than comparing motor power or purchase price. Profile producers now face tighter energy targets, unstable additive costs, and demanding surface-finish requirements. A mixer that looks impressive on paper may still produce uneven dry blends, hot spots, or excessive dust.
Grand View Research and Mordor Intelligence both identify automation, energy efficiency, and process consistency as major themes in plastics-processing machinery. Their market analyses also show continuing investment in modern equipment and production upgrades. These findings matter for PVC profile manufacturers. A reliable mixer should deliver stable heating, controlled cooling, repeatable torque, and clean discharge during long production runs.
“Extrusion is a process, not a machine,” says extrusion specialist Dr. Chris Rauwendaal. His observation applies directly to mixer selection. The mixer, extruder, formulation, and operator must work as one system. A high-speed unit cannot compensate for poor temperature control or inaccurate dosing. Not always.
This guide compares the factors that genuinely influence performance, including batch capacity, rotor design, thermal control, mixing time, maintenance access, and after-sales support. It also considers practical details, such as powder buildup around the lid, noisy bearings, and cleaning time between formulations. These details affect real factory costs. They are easy to underestimate.
There is no universal winner. The best Pvc Profile Mixer depends on resin formulation, profile geometry, production volume, and available floor space. This comparison uses published market research, technical principles, and realistic operating concerns. Some conclusions remain cautious, because supplier claims are not always supported by independent trials. That limitation deserves attention.
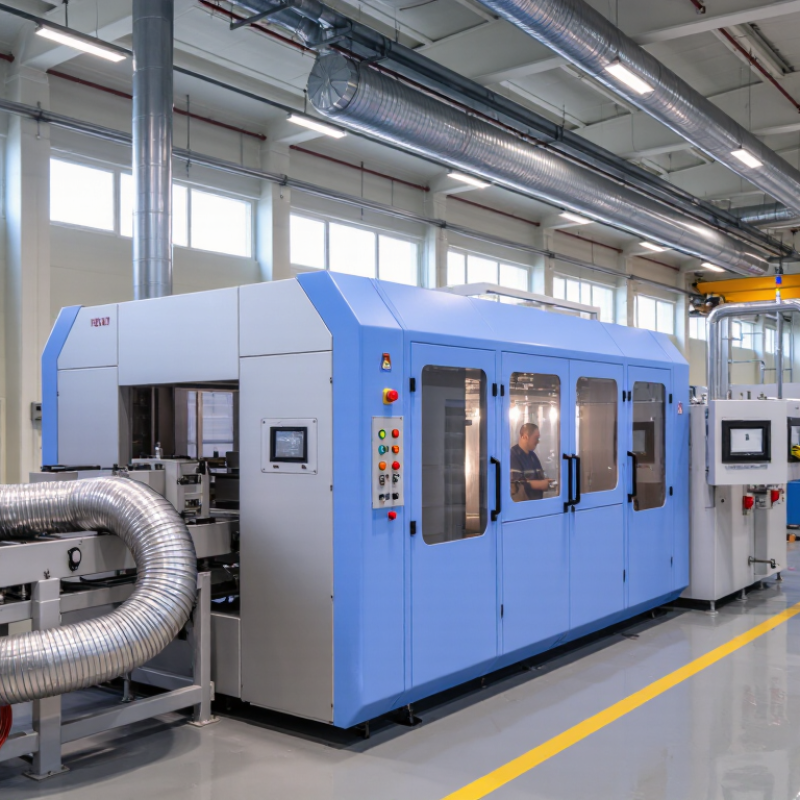
A PVC profile mixer combines resin, stabilizers, pigments, lubricants, and modifiers into a consistent dry blend. This material later enters an extruder and becomes window frames, pipes, or construction profiles. The mixer controls heat, moisture, dispersion, and batch uniformity. Small variations can create streaks, weak corners, or unstable extrusion.
In 2026, a reliable mixer needs more than a large motor. Operators should examine mixing speed, cooling efficiency, discharge time, and cleanout access. Torque monitoring can reveal unusual loads before they damage equipment. Temperature sensors also help protect heat-sensitive additives. During production evaluations, I would compare several batches, not just one. Consistent color and bulk density matter more than impressive brochure figures.
Energy use has become a practical selection factor. Efficient drive systems and shorter cycles can reduce operating costs across thousands of batches.
Automated dosing and batch records improve traceability, especially when recycled material is included. Still, automation is not always the answer. A complicated control system may slow a small factory when technicians lack proper training. That weakness is easy to overlook.
The best PVC profile mixer depends on formulation, output, floor space, and maintenance skills. A trial with the actual compound remains essential. Ask for measurable results. Fancy screens are not proof.
The best PVC profile mixer is defined by control, consistency, and practical maintenance. A strong machine should manage heating, cooling, and mixing speed with accurate sensors. Stable temperature control protects PVC powder from uneven fusion and unwanted discoloration. The mixing chamber also needs a smooth interior, since trapped material can affect the next batch. From production experience, reliable torque monitoring is essential. It shows when the material becomes too heavy or too dry.
Discharge speed matters. A clean, quick outlet reduces residue and supports steady profile production. Look for sealed bearings, accessible wear parts, and a cooling system that handles repeated cycles. Digital controls can record temperature, time, and motor load for quality checks. However, automation is not magic. Poor sensor placement can create confident but inaccurate readings. Operators still need to inspect the blend, listen for unusual vibration, and compare results between batches. Small details often expose larger problems.
Tips: Test the mixer with your actual PVC formulation before purchasing. Check noise, discharge cleanliness, temperature recovery, and energy use. Ask for maintenance records and service training. Do not choose the highest capacity automatically. An oversized mixer may waste energy and produce inconsistent smaller batches. The right model should match your output, material behavior, floor space, and team’s operating skills. Safety guards and emergency stops must be easy to reach. They should never be treated as optional features.
What Is the Best PVC Profile Mixer in 2026?
How to Compare PVC Profile Mixer Types and Specifications
The best PVC profile mixer depends on output, formulation, and temperature control. A high-speed hot mixer disperses stabilizers quickly and supports consistent plasticization. A separate cooling mixer then reduces the compound temperature before extrusion. Integrated systems save floor space, but they can complicate maintenance. Choose by production evidence, not brochure speed.
Grand View Research estimated the global PVC market at about USD 45 billion in 2023. PlasticsEurope reported 413.8 million tonnes of global plastics production in 2023. These figures suggest strong demand, but they do not justify buying the largest mixer. Compare usable batch volume, rotor speed, motor power, heating method, cooling efficiency, and discharge temperature. In plant trials, a stable discharge temperature often matters more than maximum rpm. Higher speed can also increase heat and material degradation.
Tips: Request a three-day material trial. Record batch time, energy use, temperature variation, dust release, and cleaning time. Check whether the mixer handles calcium carbonate, stabilizers, and recycled content without dead zones. Ask for service records and verified performance data. A smaller mixer may be better for frequent color changes. That choice is easy to underestimate.
How to compare PVC profile mixer types and specifications based on typical practical throughput ranges.
For most PVC profile production lines, a hot-and-cold mixer unit is generally the most balanced option because it combines efficient heat mixing with rapid cooling before extrusion. The ranges shown are typical industry specification ranges for PVC dry-blend preparation; actual throughput depends on batch volume, formulation, moisture level, mixing temperature, cycle time, and automation.
Choosing the best PVC profile mixer in 2026 starts with materials, not marketing claims. Rigid PVC profiles often contain calcium carbonate, titanium dioxide, stabilizers, lubricants, and impact modifiers. Each additive changes torque, heat transfer, and mixing time. A formulation with higher mineral loading needs stronger shear and a more durable mixing chamber.
PlasticsEurope’s Plastics—the Fast Facts 2024 report places PVC at about 9.8% of European plastics demand. That share matters because profile producers face varied recipes, from virgin compounds to formulations with recycled PVC. A suitable system should provide accurate temperature control, repeatable batching, and gentle cooling. Overheating can cause discoloration and reduce impact performance. Small details matter.
Production scale also shapes the decision. A high-volume line may need a hot mixer paired with a dedicated cooling mixer, while a smaller workshop may value flexible batch sizes and faster cleaning. The mixer should match extrusion output, not merely its advertised capacity. Check motor torque, rotor design, dust extraction, maintenance access, and energy use per batch. The European Commission’s Best Available Techniques reference for plastics processing emphasizes process control and energy efficiency, but the ideal setting still depends on local conditions. There is no universal best machine. A rushed selection can look efficient on paper and fail during seasonal humidity changes or recycled-material fluctuations. Hands-on trials remain essential.
| Mixer Configuration | Best-Matched PVC Material | Typical Working Volume | Typical Discharge Temperature | Suitable Production Scale | Main Advantages | Main Limitations | Fit Score |
|---|---|---|---|---|---|---|---|
| High-Speed Hot Mixer with Cooling Mixer | Rigid PVC dry blends containing PVC resin, stabilizer, lubricant, impact modifier, processing aid, filler and pigment | 50–1,000 L per hot-mixing vessel; cooling vessel commonly paired at 1.5–3 times hot-vessel volume | Hot mix: approximately 110–125°C; cooled blend: approximately 40–50°C | Small, medium and high-volume profile extrusion lines | Strong dispersion, repeatable dry blending, short cycle time and good compatibility with automated dosing | Requires accurate temperature control, dust management and correct hot-to-cold vessel matching | 9.5/10 |
| Low-Speed Intensive Mixer | Rigid PVC compounds with moderate filler levels and formulations that require gentle heat development | 100–800 L per batch | Typically 90–115°C, depending on formulation and shear level | Low- to medium-volume profile production | Lower mechanical stress, relatively simple operation and suitable for controlled batch processing | Longer mixing cycles and generally lower dispersion efficiency than high-speed systems | 7.5/10 |
| High-Intensity Mixer with Direct Cooling | Rigid PVC profiles with higher filler content, dense additives or demanding color consistency | 100–1,500 L per batch, subject to rotor design and motor power | Hot mix: approximately 110–130°C; direct cooling used to prevent over-heating | Medium- to high-volume production with frequent formulation changes | High shear, fast additive coating, effective filler distribution and strong batch-to-batch consistency | Higher power demand, greater wear risk and more demanding maintenance requirements | 9.0/10 |
| Two-Stage Hot and Cold Mixing Unit | General-purpose rigid PVC dry blends for window profiles, door profiles, siding and technical sections | Common batch sizes: 100–1,000 kg, depending on vessel volume and bulk density | Hot mix commonly 110–125°C; cold discharge commonly below 50°C | Continuous multi-shift extrusion plants | Good thermal stability, efficient cooling, high throughput and reduced risk of premature fusion | Higher initial investment and larger floor-space requirement than a single-vessel mixer | 9.8/10 |
| Laboratory or Pilot Mixer | New PVC formulations, recycled-content trials, color development and process validation | 2–50 L per batch | Adjustable; commonly tested within 80–130°C | Research, development and small-batch production | Low material consumption, fast formulation changeover and useful for scale-up testing | Not economical for high-throughput production and may not reproduce full-scale heat-transfer behavior | 6.5/10 |
| Recycling-Focused Hot Mixer | PVC regrind blends containing controlled proportions of post-industrial or post-consumer material | 100–800 L per batch, depending on bulk density and feed consistency | Typically controlled below the formulation’s degradation limit; often approximately 95–120°C | Medium-scale production using recycled feedstock | Supports regrind incorporation, homogenizes variable feedstock and can reduce virgin-material consumption | Requires strict contaminant control, moisture management and formulation adjustment | 8.2/10 |
I have seen factories choose oversized mixers for future growth. The result was uneven additive distribution and unnecessary energy use. Check the heating and cooling system carefully. Water temperature should remain stable during each cycle. The mixer also needs sufficient torque for rigid PVC compounds, especially when fillers increase material resistance. Ask for trial mixing with your own resin, stabilizer, pigment, and calcium carbonate. Inspect the powder after discharge. It should look uniform, without visible color streaks or hard lumps.
Practical maintenance details often decide long-term value. Examine the blade surface, sealing points, discharge valve, and cleaning access. Operators should reach inspection areas without unsafe climbing or awkward tools. Review electrical protection, emergency stops, guarding, and documented safety compliance. Reliable suppliers should provide test records, operating instructions, spare-parts information, and service response terms. These details matter.
| Cookie | Duration | Description |
|---|---|---|
| AWSALB | 7 days | AWSALB is a cookie generated by the Application load balancer in the Amazon Web Services. It works slightly different from AWSELB. |
| AWSALBCORS | 7 days | This cookie is used for load balancing services provded by Amazon inorder to optimize the user experience. Amazon has updated the ALB and CLB so that customers can continue to use the CORS request with stickness. |
| cookielawinfo-checkbox-advertisement | 1 year | The cookie is set by GDPR cookie consent to record the user consent for the cookies in the category "Advertisement". |
| cookielawinfo-checkbox-analytics | 11 months | This cookie is set by GDPR Cookie Consent plugin. The cookie is used to store the user consent for the cookies in the category "Analytic / Performance". |
| cookielawinfo-checkbox-functional | 11 months | The cookie is set by GDPR cookie consent to record the user consent for the cookies in the category "Functional". |
| cookielawinfo-checkbox-necessary | 11 months | This cookie is set by GDPR Cookie Consent plugin. The cookies is used to store the user consent for the cookies in the category "Strictly Necessary". |
| cookielawinfo-checkbox-performance | 11 months | This cookie is set by GDPR Cookie Consent plugin. The cookie is used to store the user consent for the cookies in the category "Performance". |
| cookielawinfo-checkbox-preferences | 11 months | This cookie is set by GDPR Cookie Consent plugin. The cookie is used to store the user consent for the cookies in the category "Preferences." |
| elementor | never | This cookie is used by the website's WordPress theme. It allows the website owner to implement or change the website's content in real-time. |
| viewed_cookie_policy | 11 months | The cookie is set by the GDPR Cookie Consent plugin and is used to store whether or not user has consented to the use of cookies. It does not store any personal data. |
| Cookie | Duration | Description |
|---|---|---|
| CONSENT | 16 years 4 months | These cookies are set via embedded youtube-videos. They register anonymous statistical data on for example how many times the video is displayed and what settings are used for playback.No sensitive data is collected unless you log in to your google account, in that case your choices are linked with your account, for example if you click “like” on a video. |
| _ga | 2 years | This cookie is installed by Google Analytics. The cookie is used to calculate visitor, session, campaign data and keep track of site usage for the site's analytics report. The cookies store information anonymously and assign a randomly generated number to identify unique visitors. |
| _gat_gtag_UA_47200144_1 | 1 minute | This cookie is set by Google and is used to distinguish users. |
| _gid | 1 day | This cookie is installed by Google Analytics. The cookie is used to store information of how visitors use a website and helps in creating an analytics report of how the website is doing. The data collected including the number visitors, the source where they have come from, and the pages visted in an anonymous form. |
| _hjAbsoluteSessionInProgress | session | This cookie is used to count how many times a website has been visited by different visitors. This is done by assigning the visitor an ID, so the visitor does not get registered twice. |
| _hjFirstSeen | 30 minutes | This is set by Hotjar to identify a new user’s first session. It stores a true/false value, indicating whether this was the first time Hotjar saw this user. It is used by Recording filters to identify new user sessions. |
| _hjid | 1 year | This cookie is set by Hotjar. This cookie is set when the customer first lands on a page with the Hotjar script. It is used to persist the random user ID, unique to that site on the browser. This ensures that behavior in subsequent visits to the same site will be attributed to the same user ID. |
| _hjIncludedInPageviewSample | session | This cookie is used to detect whether the user navigation and interactions are included in the website’s data analytics. |
| Cookie | Duration | Description |
|---|---|---|
| IDE | 1 year 24 days | This cookie is used by Google DoubleClick and stores information about how the user uses the website and any other advertisement before visiting the website. This is used to present users with ads that are relevant to them according to the user profile. |
| NID | 6 months | This cookie is used to a profile based on user's interest and display personalized ads to the users. |
| test_cookie | 15 minutes | This cookie is set by doubleclick.net. The purpose of the cookie is to determine if the user's browser supports cookies. |
| VISITOR_INFO1_LIVE | 5 months 27 days | This cookie is set by Youtube it is used to track the information of the embedded YouTube videos on a website. |
| YSC | session | This cookies is set by Youtube and is used to track the views of embedded videos. |
| yt-remote-connected-devices | never | These cookies are set via embedded youtube-videos. |
| yt-remote-device-id | never | These cookies are set via embedded youtube-videos. |
| Cookie | Duration | Description |
|---|---|---|
| qtrans_front_language | 1 year | This cookie is set by qTranslate WordPress plugin. The cookie is used to manage the preferred language of the visitor. |