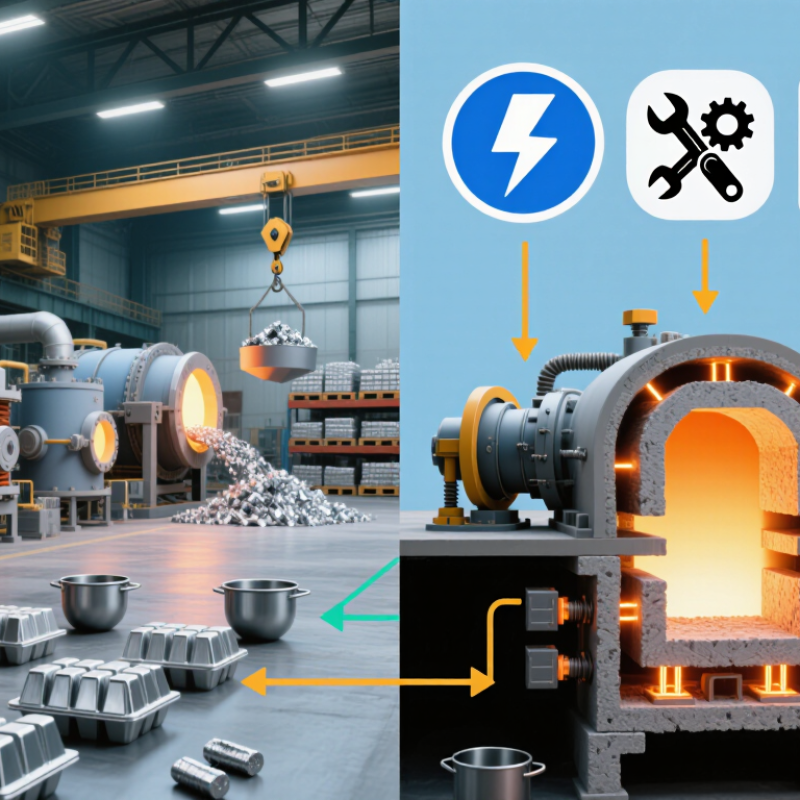
Choosing the best aluminium melting furnace requires more than comparing purchase prices. The furnace must match alloy families, batch sizes, charging methods, and production schedules. A small foundry may value flexible batch control, while a high-volume plant may need continuous melting and automatic tapping. These differences affect metal quality, energy use, labor, and maintenance.
Industry data makes the decision more urgent. The International Energy Agency reports that aluminium production consumes about 4% of global electricity. The International Aluminium Institute states that recycled aluminium requires roughly 5% of the energy used for primary aluminium production. These figures highlight the value of efficient remelting, accurate temperature control, and low metal loss. However, efficiency depends on operating conditions. Poor scrap preparation can increase oxidation, dross, and furnace time, even with advanced equipment.
Small details matter.
This guide examines fuel type, furnace capacity, thermal efficiency, refractory design, emissions control, and automation. It also considers crucible, reverberatory, rotary, and induction systems. Each aluminium melting furnace has practical strengths and limitations. Induction systems can offer precise control, but their electrical demand and metal cleanliness requirements deserve careful review. Gas-fired furnaces may provide useful capacity and flexibility, yet combustion performance and heat recovery must be evaluated. Manufacturer claims should be checked against measured fuel consumption, melt yield, temperature stability, and service records. No furnace is perfect. The best choice is the one that fits the real process, not the most impressive brochure. A careful buyer should also review regional safety standards, operator training, spare-parts availability, and total cost over the furnace’s working life.
How to Choose the Best Aluminium Melting Furnace?
Aluminium melts at 660.3°C, but furnace selection should not stop at this number. In practical workshop trials, operators often need controlled temperatures between 680°C and 760°C. The correct range depends on alloy composition, casting speed, and required fluidity. Excessive heat can increase oxidation, hydrogen absorption, and metal loss. Insufficient heat may cause poor filling and visible casting defects. That margin matters.
Different alloys require different thermal treatment. Some casting alloys need careful holding temperatures to protect magnesium or other reactive elements. A furnace should provide stable heating, accurate temperature measurement, and enough capacity for your batch size. Consider fuel efficiency, crucible compatibility, exhaust control, and ease of cleaning. A furnace that melts quickly may still perform poorly if its temperature fluctuates during holding. This is where selection becomes less obvious.
Tips: Measure the metal, not only the furnace chamber. Use a calibrated thermocouple and record melting times for each alloy. Keep the crucible clean and remove oxide carefully. Avoid unnecessary superheating, even when production is behind schedule. Review your results after every batch. Some assumptions will be wrong. A modest furnace with steady control can outperform a larger unit operated without discipline. Always confirm alloy data through technical standards or qualified metallurgical advice before changing process temperatures.
Aluminium alloys melt across different temperature ranges. Pure aluminium melts at 660.3°C, while alloying elements can lower the solidus temperature and widen the melting range. Furnace selection should therefore consider the alloy, batch size, heating uniformity, temperature control and required superheat.
How to read the chart: The solidus temperature is where melting begins, while the liquidus temperature is where the alloy becomes fully liquid. The values shown are approximate and can vary with alloy composition and material specification.
Capacity planning should start with metal demand, not furnace size. A 500 kg batch furnace may suit job shops, casting trials, or irregular orders. At one 90-minute cycle, its theoretical output is only 0.33 t/h. Charging, skimming, temperature checks, and transfer reduce this figure further. Real plants rarely achieve nameplate capacity. A spreadsheet can still mislead.
For 10 t/h production, calculate backward from usable molten aluminium. With an 88% metal yield and 85% operating availability, the furnace system may need approximately 13.4 t/h of rated capacity. That could mean several batch furnaces, or a continuous melting and holding arrangement. The choice depends on scrap form, alloy changes, furnace loading, and delivery distance. The International Aluminium Institute states that recycled aluminium can require up to 95% less energy than primary aluminium, but contaminated scrap can increase dross and processing losses. Capacity alone does not guarantee efficiency.
Tips: Record actual cycle times for two weeks. Measure charging delays, dross, temperature correction, and idle hours. Leave expansion space, but avoid buying capacity that will remain cold. A 500 kg unit may be ideal today, yet restrictive after one major contract. Conversely, a 10 t/h system can become expensive overhead when demand is seasonal. Discuss these risks with an experienced furnace engineer and verify performance data under your real alloy mix.
A practical furnace comparison begins with energy use, not purchase price. Modern operations often target 550–750 kWh per ton of aluminium melted. The lower figure is achievable. However, it requires dry charge material, stable loading, and limited heat loss. In plant trials, operators should record gas or electricity consumption beside actual aluminium output. This prevents misleading results caused by holding metal, idle time, or incomplete batches. Measure the whole process.
Furnace design strongly affects this range. A well-insulated chamber reduces heat escaping through doors and walls. Precise burner control can also shorten melting cycles. Charge size matters too. Cold, mixed scrap usually needs more energy than clean, preheated ingots. A furnace using 600 kWh per ton may appear efficient, but the result changes if the measurement excludes warm-up energy. That is a common weakness. Ask for test conditions, weighing methods, and operating temperatures before accepting performance claims.
Tips: Install a separate energy meter for each furnace. Track kWh per ton weekly, not only during ideal production days. Inspect door seals and refractory surfaces regularly. Keep loading doors closed between charges. Review dross levels, because excessive oxidation can hide energy losses. A simple spreadsheet often reveals patterns faster than a sales brochure. Leave room for human error. Operators may load unevenly, and real factories rarely match laboratory conditions.
Fuel, electric, induction, and holding furnaces suit different production realities. Gas-fired furnaces remain practical for large batches and heavy crucibles. Their flame heats the chamber directly, but exhaust losses can be significant.
Electric resistance furnaces offer clean, controllable heating and simple temperature programming. They are useful where electricity is stable and emissions at the workshop matter. Induction furnaces heat the metal itself, often achieving fast melting and strong temperature uniformity. They require higher electrical infrastructure and careful coil maintenance.
Holding systems are different. They preserve molten aluminium between batches, reducing repeated melting cycles and oxidation. The International Aluminium Institute states that recycled aluminium requires about 5% of the energy used for primary aluminium production. Efficient holding can help protect that advantage, although electricity still has an environmental cost.
My first instinct was to choose induction. That was too simple.
A furnace should be judged by batch size, alloy change frequency, melt-loss records, energy tariffs, ventilation, and operator experience.
A small foundry may gain more from a well-insulated electric furnace than an oversized induction unit.
Measure the real cycle. Forecasts alone can mislead.
A reliable furnace should target metal recovery above 90%, but this figure needs careful definition. Is recovery measured after melting, or after dross treatment? Clean, dry scrap usually performs better than painted or oily feedstock. In practical audits, weigh the charge, molten output, dross, and residues every shift. Measure it daily.
A 2023 report from the International Aluminium Institute states that recycling aluminium uses about 95% less energy than primary production. However, excessive holding time can increase oxidation and reduce that advantage.
Emissions deserve equal attention. Ask for measured particulate, nitrogen oxide, and volatile organic compound data, not only catalogue estimates. The US EPA AP-42 guidance identifies furnace charging, melting, and dross handling as important emission points.
A furnace with sealed charging, effective extraction, and suitable filtration can improve workplace air quality. Still, one oversized filter does not solve poor airflow design. Operators should also inspect alarms, door interlocks, emergency stops, and molten-metal containment. Safety is measurable.
Cost calculations should include electricity, refractory replacement, maintenance, labour, and metal loss. European Aluminium’s Environmental Profile Report 2022 shows the major carbon advantage of recycled aluminium, yet energy performance varies by feedstock and process control.
A cheaper furnace may look attractive initially. It may become expensive through unstable temperature control and higher dross generation. Request verified operating data from comparable loads, then test the assumptions with a short production trial. A spreadsheet can still mislead.
| Cookie | Duration | Description |
|---|---|---|
| AWSALB | 7 days | AWSALB is a cookie generated by the Application load balancer in the Amazon Web Services. It works slightly different from AWSELB. |
| AWSALBCORS | 7 days | This cookie is used for load balancing services provded by Amazon inorder to optimize the user experience. Amazon has updated the ALB and CLB so that customers can continue to use the CORS request with stickness. |
| cookielawinfo-checkbox-advertisement | 1 year | The cookie is set by GDPR cookie consent to record the user consent for the cookies in the category "Advertisement". |
| cookielawinfo-checkbox-analytics | 11 months | This cookie is set by GDPR Cookie Consent plugin. The cookie is used to store the user consent for the cookies in the category "Analytic / Performance". |
| cookielawinfo-checkbox-functional | 11 months | The cookie is set by GDPR cookie consent to record the user consent for the cookies in the category "Functional". |
| cookielawinfo-checkbox-necessary | 11 months | This cookie is set by GDPR Cookie Consent plugin. The cookies is used to store the user consent for the cookies in the category "Strictly Necessary". |
| cookielawinfo-checkbox-performance | 11 months | This cookie is set by GDPR Cookie Consent plugin. The cookie is used to store the user consent for the cookies in the category "Performance". |
| cookielawinfo-checkbox-preferences | 11 months | This cookie is set by GDPR Cookie Consent plugin. The cookie is used to store the user consent for the cookies in the category "Preferences." |
| elementor | never | This cookie is used by the website's WordPress theme. It allows the website owner to implement or change the website's content in real-time. |
| viewed_cookie_policy | 11 months | The cookie is set by the GDPR Cookie Consent plugin and is used to store whether or not user has consented to the use of cookies. It does not store any personal data. |
| Cookie | Duration | Description |
|---|---|---|
| CONSENT | 16 years 4 months | These cookies are set via embedded youtube-videos. They register anonymous statistical data on for example how many times the video is displayed and what settings are used for playback.No sensitive data is collected unless you log in to your google account, in that case your choices are linked with your account, for example if you click “like” on a video. |
| _ga | 2 years | This cookie is installed by Google Analytics. The cookie is used to calculate visitor, session, campaign data and keep track of site usage for the site's analytics report. The cookies store information anonymously and assign a randomly generated number to identify unique visitors. |
| _gat_gtag_UA_47200144_1 | 1 minute | This cookie is set by Google and is used to distinguish users. |
| _gid | 1 day | This cookie is installed by Google Analytics. The cookie is used to store information of how visitors use a website and helps in creating an analytics report of how the website is doing. The data collected including the number visitors, the source where they have come from, and the pages visted in an anonymous form. |
| _hjAbsoluteSessionInProgress | session | This cookie is used to count how many times a website has been visited by different visitors. This is done by assigning the visitor an ID, so the visitor does not get registered twice. |
| _hjFirstSeen | 30 minutes | This is set by Hotjar to identify a new user’s first session. It stores a true/false value, indicating whether this was the first time Hotjar saw this user. It is used by Recording filters to identify new user sessions. |
| _hjid | 1 year | This cookie is set by Hotjar. This cookie is set when the customer first lands on a page with the Hotjar script. It is used to persist the random user ID, unique to that site on the browser. This ensures that behavior in subsequent visits to the same site will be attributed to the same user ID. |
| _hjIncludedInPageviewSample | session | This cookie is used to detect whether the user navigation and interactions are included in the website’s data analytics. |
| Cookie | Duration | Description |
|---|---|---|
| IDE | 1 year 24 days | This cookie is used by Google DoubleClick and stores information about how the user uses the website and any other advertisement before visiting the website. This is used to present users with ads that are relevant to them according to the user profile. |
| NID | 6 months | This cookie is used to a profile based on user's interest and display personalized ads to the users. |
| test_cookie | 15 minutes | This cookie is set by doubleclick.net. The purpose of the cookie is to determine if the user's browser supports cookies. |
| VISITOR_INFO1_LIVE | 5 months 27 days | This cookie is set by Youtube it is used to track the information of the embedded YouTube videos on a website. |
| YSC | session | This cookies is set by Youtube and is used to track the views of embedded videos. |
| yt-remote-connected-devices | never | These cookies are set via embedded youtube-videos. |
| yt-remote-device-id | never | These cookies are set via embedded youtube-videos. |
| Cookie | Duration | Description |
|---|---|---|
| qtrans_front_language | 1 year | This cookie is set by qTranslate WordPress plugin. The cookie is used to manage the preferred language of the visitor. |