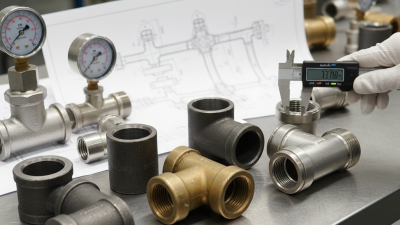
Choosing socket weld fittings is not a clerical task. It affects pressure control, leak prevention, maintenance access, and long-term plant safety. A fitting may look small, yet it becomes part of a demanding system carrying steam, chemicals, gas, or high-temperature fluids.
Piping engineer Mohinder L. Nayyar is associated with a practical design principle: “Safety, economy, and maintainability must meet in the design.” That idea is useful here. The lowest purchase price may create higher welding, inspection, or replacement costs later. Sometimes, the cheaper choice is not cheaper.
This guide explains how to select socket weld fittings with greater confidence. It considers pipe size, pressure class, temperature, material compatibility, corrosion exposure, and applicable standards such as ASME B16.11. It also examines the details that are easy to overlook, including socket depth, weld clearance, wall thickness, and access for inspection.
In real projects, drawings can be incomplete. Site dimensions may differ slightly. A supplier’s catalog may simplify an important limitation. These gaps require careful checking, not assumptions. Confirm the fitting material against the pipe specification. Review the welding procedure. Check whether the selected class suits both pressure and temperature.
Small details matter.
A reliable selection process also includes traceability, dimensional verification, and quality documentation. Even experienced engineers can miss a mismatch when schedules become tight. That is an uncomfortable truth, but it deserves attention. The right socket weld fittings should fit the design, the installation method, and the conditions expected years after commissioning.
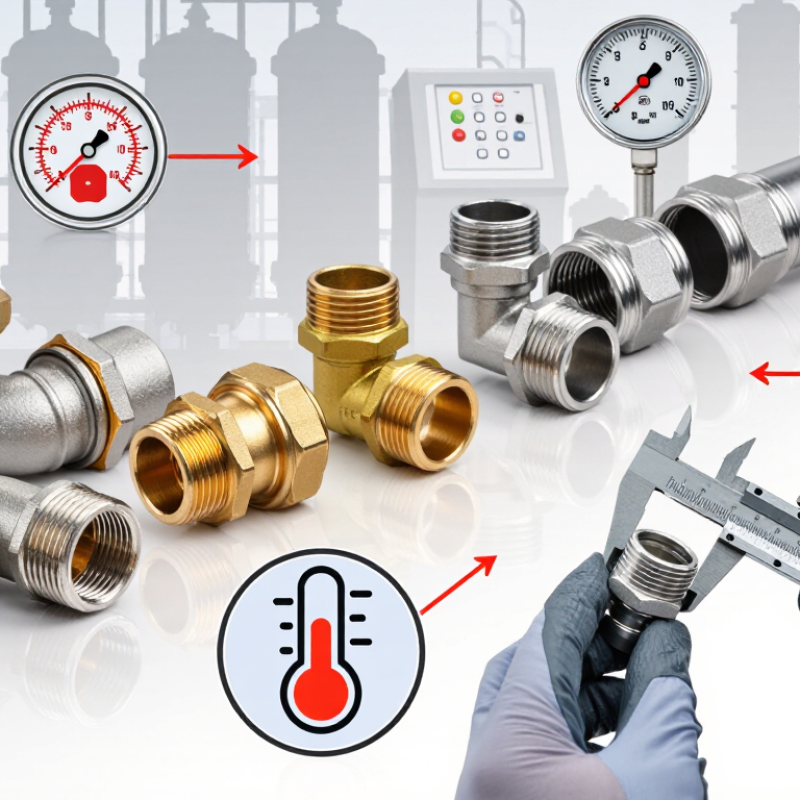
Socket weld fittings connect pipe inside a recessed socket, then use a fillet weld around the joint. This arrangement creates a compact connection with a smooth external profile. It works well in small-bore piping, instrument lines, hydraulic systems, and high-pressure services. Tight spaces often make this design practical.
Before choosing one, check the pipe outside diameter, wall thickness, material, pressure, and operating temperature. The fitting must match the piping specification, not only the visible dimensions. A stainless fitting may resist corrosion, while carbon steel may suit dry utility service. Chemical compatibility still requires careful review. Seemingly minor differences matter.
Installation quality strongly affects reliability. The pipe should be cleaned, aligned, and inserted to the specified depth. A small expansion gap is normally required, but the exact value depends on the applicable standard and procedure. Excessive insertion can create stress during heating. Poor welding may trap residue or produce incomplete fusion. Field inspections often find preparation errors before they find material defects.
I would not treat socket weld fittings as a universal solution. They can be unsuitable where internal crevices, frequent thermal cycling, or later disassembly create problems. Engineers should verify design calculations, welding qualifications, inspection requirements, and service history. In demanding systems, radiographic or other non-destructive examination may be necessary. A fitting that looks correct can still fail under vibration, corrosion, or repeated temperature changes.
How to Choose Socket Weld Fittings for Your Project?
Defining project requirements starts with the fluid, not the fitting. Record its chemical composition, concentration, viscosity, and cleanliness. Water, steam, oxygen, and corrosive chemicals create very different service demands. Note the normal and maximum pressure, temperature, flow rate, and pressure fluctuations. A fitting suitable for steady water service may fail under repeated thermal cycling. Do not guess. Verify operating data with process engineers and current piping documents.
Match the fitting material to the pipe and the conveyed medium. Check wall thickness, pipe schedule, bore size, and required pressure rating. The socket depth must suit the pipe outside diameter and installation procedure. Allow space for welding, inspection, insulation, and future maintenance. Tight equipment layouts often look acceptable on paper. They can become difficult on site. Measure twice.
Consider vibration, thermal expansion, external loads, and drainage requirements. Dead legs may trap fluid and increase corrosion or contamination risks. For high-temperature systems, review weld quality controls and heat treatment requirements. Confirm the applicable design code, inspection method, and material certificates before purchasing. I have seen projects focus heavily on nominal size while overlooking cleaning requirements or startup conditions. That omission can force expensive changes later. Recheck assumptions when the process changes.
Material selection should begin with the fluid, temperature, and surrounding environment. Carbon steel may suit dry air or standard water service. Stainless steel performs better when corrosion or contamination is a concern. For chemical service, confirm compatibility with the actual concentration and operating temperature. A fitting can look suitable and still fail through pitting or stress corrosion.
Size matching requires more than checking the pipe diameter. Verify the fitting bore, pipe schedule, wall thickness, and socket depth. A two-inch pipe with a heavier schedule may not fit every two-inch fitting correctly. Check the dimensional requirements in ASME B16.11 and the pipe specification before ordering. Leave the recommended expansion gap during welding. It reduces stress, although installers sometimes overlook it on crowded lines.
Pressure ratings must match both pressure and temperature. A 3,000-class fitting does not automatically provide the same rating at elevated heat. Use the manufacturer’s pressure-temperature tables and the applicable material standard. Consider pressure surges, vibration, and repeated thermal cycling. These conditions can weaken a connection over time. Also check whether the selected metal requires special welding procedures or inspection. A quick catalog choice is tempting, but it may ignore corrosion allowance or future operating changes. Rechecking the calculation is worthwhile.
How to Choose Socket Weld Fittings for Your Project?
Choosing socket weld fittings starts with the applicable standard, not the lowest price. Confirm requirements such as ASME B16.11, ASTM material specifications, or project-specific codes. Check pressure ratings at the actual operating temperature. A fitting may meet one standard but fail your project’s documentation requirements. Request material certificates, heat numbers, and inspection records before installation.
Compatibility needs careful attention. Match the fitting material with the pipe, process fluid, temperature range, and corrosion conditions. Verify pipe outside diameter and wall thickness. The socket depth should allow the recommended expansion gap during welding. Without this gap, thermal expansion can create stress and cracking. In field inspections, poor cleaning and inaccurate fit-up appear more often than expected. That detail is easy to underestimate. Connection quality also depends on a qualified welding procedure, controlled heat input, and a clean joint. Visual inspection may detect poor alignment, but critical systems may require additional nondestructive testing.
Tips: Compare standards line by line. Check the pipe schedule. Keep the socket gap consistent. Record each fitting’s heat number. Do not assume a certified fitting suits every service. Recheck the specification when conditions change. Small deviations can become expensive failures.
Choosing socket weld fittings starts with the installation environment, not the catalog photograph. Confirm pipe size, wall thickness, pressure, temperature, and fluid compatibility. The fitting must match the piping material and applicable design code. Keep it practical. Is the line accessible for welding and inspection? Tight spaces may favor socket welds, but poor access can increase workmanship risks. Leave the specified socket gap for thermal movement and proper welding. A small gap matters. Clean, square pipe ends help prevent misalignment and trapped contaminants. Ask the fabricator about welding procedures, qualifications, and required examinations before purchasing.
Cost estimates should include more than fitting prices. Labor, cutting, preparation, cleaning, welding, inspection, and pressure testing can change the final figure. Socket welds often simplify small-bore installation, yet they may cost more when access is difficult. Stainless or high-alloy materials also raise purchase and welding costs. Compare the installed cost, not the unit cost. In one field review, an inexpensive fitting caused delays because its dimensions did not suit existing pipe supports. That mistake was avoidable. I should have checked the as-built measurements earlier.
Long-term performance depends on service conditions and installation discipline. Check corrosion resistance, vibration, thermal cycling, and dead-leg concerns before selection. Avoid socket weld fittings where repeated flexing could stress the joint. Support nearby piping so the weld carries no unnecessary loads. Record heat numbers, inspection results, and test records for future maintenance. Periodic inspection is useful around dissimilar metals and vibrating equipment. No selection is perfect. Recheck assumptions when the process changes, even slightly. A fitting that performs well today may fail after temperature, chemistry, or operating pressure changes.
| Decision Criterion | Carbon Steel Socket Weld Fittings | 304 Stainless Steel Socket Weld Fittings | 316 Stainless Steel Socket Weld Fittings | Alloy Steel Socket Weld Fittings | Project Selection Guidance |
|---|---|---|---|---|---|
| Common Material Specifications | Forged carbon steel commonly supplied to ASTM A105 or equivalent requirements. | Forged austenitic stainless steel commonly supplied to ASTM A182 F304 or F304L requirements. | Forged austenitic stainless steel commonly supplied to ASTM A182 F316 or F316L requirements. | Low-alloy forged steel commonly supplied to ASTM A182 F11 or F22 requirements. | Confirm the fitting material matches the pipe, weld procedure, design code, fluid service, and required material certificates. |
| Typical Service | General industrial utilities, compressed air, water, oil, steam, and non-corrosive process lines. | Food, pharmaceutical, clean utility, water, and moderately corrosive process services. | Chloride-containing, marine, chemical, and more corrosive environments than 304 stainless steel. | Elevated-temperature and high-pressure steam, boiler, power-generation, and high-temperature hydrocarbon systems. | Choose by actual fluid chemistry, temperature, pressure, corrosion risk, and applicable piping code rather than by material price alone. |
| Size Range to Verify | Socket weld fittings are commonly used in small-bore piping; many forged fitting standards cover NPS 1/8 through NPS 4. | Often selected for small-bore hygienic or corrosive process piping within the project’s specified size range. | Often selected for small-bore chloride or marine-service piping within the project’s specified size range. | Commonly used in small-bore high-temperature systems, subject to the applicable dimensional standard. | Check the approved standard, fitting schedule, outside diameter, wall thickness, and availability for every nominal pipe size. |
| Pressure and Temperature Rating | Pressure capability depends on the fitting class, material, temperature, wall thickness, and design code; do not select by nominal size alone. | Rating decreases at elevated temperature and must be checked against the material and applicable pressure-temperature tables. | Generally offers improved resistance to chloride-related corrosion, but pressure-temperature limits still require verification. | Suitable for elevated-temperature service when the specified grade, heat treatment, and allowable stresses are approved for the design conditions. | Compare design pressure and temperature with the complete pressure-temperature rating. The piping system rating is governed by its weakest component. |
| Installation Requirements | Requires accurate pipe insertion, proper alignment, qualified socket-weld procedures, and protection against contamination and moisture. | Requires clean tools and controlled heat input to reduce discoloration, distortion, and contamination during welding. | Requires careful cleaning and heat control because contamination and poor weld practice can reduce corrosion resistance. | Usually requires stricter welding controls, qualified procedures, preheating, and post-weld heat treatment where specified by the code or procedure. | Provide the socket-weld gap specified by the governing code or project procedure; a commonly used value is approximately 1/16 in (1.6 mm), but the approved procedure controls. |
| Inspection and Testing | Visual inspection is standard; radiographic, dye penetrant, magnetic particle, hydrostatic, or pneumatic testing may be required by the code and service. | Visual inspection and dye penetrant testing may be used when surface cracking or weld quality requires additional examination. | Inspection may include dye penetrant testing and corrosion-focused quality controls for critical service. | Weld procedure qualification, welder qualification, hardness checks, heat-treatment records, and nondestructive examination may be required. | Define inspection levels before purchasing. Critical, cyclic, toxic, flammable, or high-temperature services generally require more documentation and examination. |
| Relative Material Cost | Low: typically the lowest material-cost option when corrosion protection is not required. | Medium to high: higher initial cost than carbon steel because of alloy content and manufacturing requirements. | High: generally costs more than 304 stainless steel because of increased nickel and molybdenum content. | Medium to high: cost varies with grade, heat treatment, certification, and high-temperature service requirements. | Use relative cost for early screening only. Include welding consumables, preheat, heat treatment, inspection, coatings, installation time, and replacement risk in the total cost. |
| Corrosion Performance | Low to moderate in corrosive environments; often needs coating, lining, corrosion allowance, or chemical control. | Good general corrosion resistance, but it can be vulnerable to chloride environments and some reducing acids. | Better resistance than 304 stainless steel to many chloride and pitting conditions, but it is not immune to corrosion. | Designed primarily for strength at elevated temperature; corrosion resistance depends strongly on the specific alloy and service chemistry. | Evaluate pitting, crevice corrosion, stress-corrosion cracking, erosion, galvanic effects, and external atmospheric exposure. |
| Long-Term Maintenance | May require coating renewal, corrosion monitoring, thickness measurement, and more frequent replacement in aggressive service. | Usually requires less external coating maintenance, but cleaning practices and chloride exposure must be controlled. | Can reduce corrosion-related maintenance in suitable chloride services, while still requiring inspection and correct cleaning. | Requires monitoring of creep, fatigue, oxidation, weld condition, and heat-treatment compliance in high-temperature service. | Select the material with the lowest whole-life cost, not simply the lowest purchase price. Consider access, shutdown cost, safety, and expected service life. |
| Best Fit for the Project | Budget-sensitive, non-corrosive, moderate-temperature systems with practical access for coating or inspection. | Clean or moderately corrosive systems where general stainless performance is adequate. | Process, marine, or chloride-bearing systems where improved pitting resistance is justified. | High-temperature and high-pressure systems requiring elevated-temperature strength and controlled welding. | Before approval, verify standard, material grade, fitting class, dimensions, wall thickness, end preparation, certificates, welding procedure, inspection plan, and delivery schedule. |
| Cookie | Duration | Description |
|---|---|---|
| AWSALB | 7 days | AWSALB is a cookie generated by the Application load balancer in the Amazon Web Services. It works slightly different from AWSELB. |
| AWSALBCORS | 7 days | This cookie is used for load balancing services provded by Amazon inorder to optimize the user experience. Amazon has updated the ALB and CLB so that customers can continue to use the CORS request with stickness. |
| cookielawinfo-checkbox-advertisement | 1 year | The cookie is set by GDPR cookie consent to record the user consent for the cookies in the category "Advertisement". |
| cookielawinfo-checkbox-analytics | 11 months | This cookie is set by GDPR Cookie Consent plugin. The cookie is used to store the user consent for the cookies in the category "Analytic / Performance". |
| cookielawinfo-checkbox-functional | 11 months | The cookie is set by GDPR cookie consent to record the user consent for the cookies in the category "Functional". |
| cookielawinfo-checkbox-necessary | 11 months | This cookie is set by GDPR Cookie Consent plugin. The cookies is used to store the user consent for the cookies in the category "Strictly Necessary". |
| cookielawinfo-checkbox-performance | 11 months | This cookie is set by GDPR Cookie Consent plugin. The cookie is used to store the user consent for the cookies in the category "Performance". |
| cookielawinfo-checkbox-preferences | 11 months | This cookie is set by GDPR Cookie Consent plugin. The cookie is used to store the user consent for the cookies in the category "Preferences." |
| elementor | never | This cookie is used by the website's WordPress theme. It allows the website owner to implement or change the website's content in real-time. |
| viewed_cookie_policy | 11 months | The cookie is set by the GDPR Cookie Consent plugin and is used to store whether or not user has consented to the use of cookies. It does not store any personal data. |
| Cookie | Duration | Description |
|---|---|---|
| CONSENT | 16 years 4 months | These cookies are set via embedded youtube-videos. They register anonymous statistical data on for example how many times the video is displayed and what settings are used for playback.No sensitive data is collected unless you log in to your google account, in that case your choices are linked with your account, for example if you click “like” on a video. |
| _ga | 2 years | This cookie is installed by Google Analytics. The cookie is used to calculate visitor, session, campaign data and keep track of site usage for the site's analytics report. The cookies store information anonymously and assign a randomly generated number to identify unique visitors. |
| _gat_gtag_UA_47200144_1 | 1 minute | This cookie is set by Google and is used to distinguish users. |
| _gid | 1 day | This cookie is installed by Google Analytics. The cookie is used to store information of how visitors use a website and helps in creating an analytics report of how the website is doing. The data collected including the number visitors, the source where they have come from, and the pages visted in an anonymous form. |
| _hjAbsoluteSessionInProgress | session | This cookie is used to count how many times a website has been visited by different visitors. This is done by assigning the visitor an ID, so the visitor does not get registered twice. |
| _hjFirstSeen | 30 minutes | This is set by Hotjar to identify a new user’s first session. It stores a true/false value, indicating whether this was the first time Hotjar saw this user. It is used by Recording filters to identify new user sessions. |
| _hjid | 1 year | This cookie is set by Hotjar. This cookie is set when the customer first lands on a page with the Hotjar script. It is used to persist the random user ID, unique to that site on the browser. This ensures that behavior in subsequent visits to the same site will be attributed to the same user ID. |
| _hjIncludedInPageviewSample | session | This cookie is used to detect whether the user navigation and interactions are included in the website’s data analytics. |
| Cookie | Duration | Description |
|---|---|---|
| IDE | 1 year 24 days | This cookie is used by Google DoubleClick and stores information about how the user uses the website and any other advertisement before visiting the website. This is used to present users with ads that are relevant to them according to the user profile. |
| NID | 6 months | This cookie is used to a profile based on user's interest and display personalized ads to the users. |
| test_cookie | 15 minutes | This cookie is set by doubleclick.net. The purpose of the cookie is to determine if the user's browser supports cookies. |
| VISITOR_INFO1_LIVE | 5 months 27 days | This cookie is set by Youtube it is used to track the information of the embedded YouTube videos on a website. |
| YSC | session | This cookies is set by Youtube and is used to track the views of embedded videos. |
| yt-remote-connected-devices | never | These cookies are set via embedded youtube-videos. |
| yt-remote-device-id | never | These cookies are set via embedded youtube-videos. |
| Cookie | Duration | Description |
|---|---|---|
| qtrans_front_language | 1 year | This cookie is set by qTranslate WordPress plugin. The cookie is used to manage the preferred language of the visitor. |