Selecting the right Powder Pressing Machine manufacturer requires more than comparing catalog prices. Production managers must examine pressure stability, die compatibility, automation, maintenance, and after-sales support. A reliable machine should deliver consistent density across every compacted part. Small variations can affect strength, dimensions, and later processing.
This guide explores leading Powder Pressing Machine manufacturers worldwide and the factors that distinguish experienced suppliers. It considers hydraulic, mechanical, and servo-driven systems, along with practical details such as cycle speed, powder feeding, tooling changes, and control accuracy. Factory experience matters. So does technical evidence.
Manufacturers with strong engineering teams usually provide clearer drawings, trial pressing, and documented performance data. Their service networks can also reduce downtime when sensors fail or hydraulic seals wear. These details are easy to overlook during purchasing.
A closer look helps.
However, no manufacturer fits every production environment. A high-speed machine may suit large-volume ceramic parts but perform poorly in a small laboratory. Published specifications can also omit energy use, operator training, or long-term maintenance costs. That gap deserves attention.
The following overview aims to support careful comparison through practical, industry-focused criteria. It does not treat brand visibility as proof of quality. Instead, it considers verified capabilities, customer support, customization, safety practices, and application experience. Some comparisons remain imperfect, because manufacturers report data differently. Still, thoughtful evaluation can reveal which suppliers offer dependable value for specific materials, part sizes, and production goals.
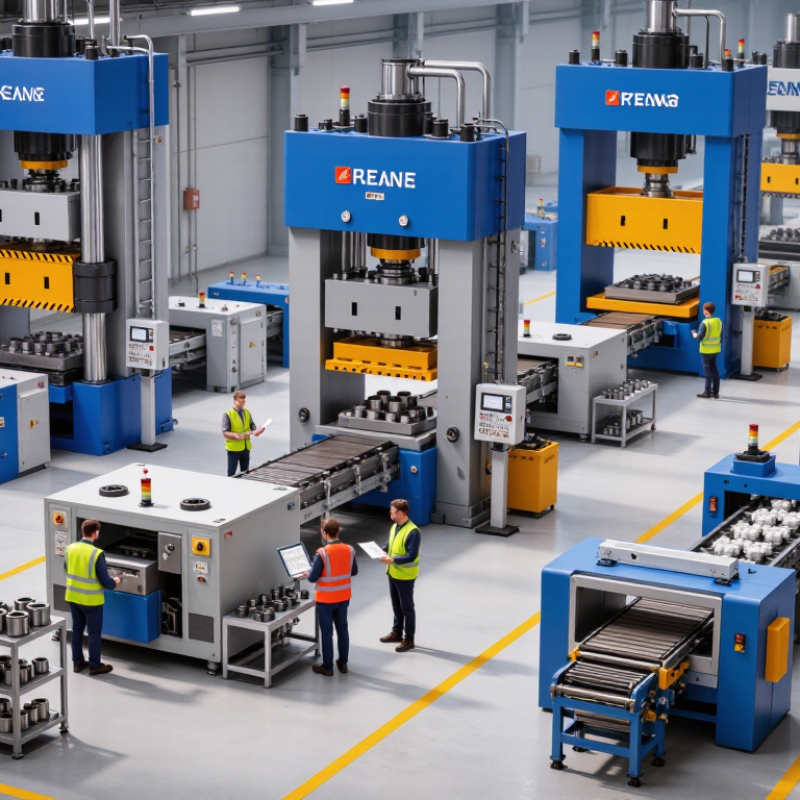
Powder pressing machines shape dry or lightly granulated powders into accurate compact parts. Common types include mechanical, hydraulic, and cold isostatic presses. Mechanical models suit fast, repeatable production. Hydraulic systems offer adjustable force and longer dwell times. Isostatic presses apply pressure more evenly around complex shapes.
The 100–1,000 MPa range covers very different manufacturing needs. Around 100 MPa may suit softer ceramic powders and preliminary compaction. Dense carbide, technical ceramic, and magnetic components can require several hundred MPa. Some demanding applications approach 1,000 MPa, but tooling strength, powder flow, and safety design become critical. Pressure is not a quality guarantee.
Small details matter. A controlled filling system reduces weight variation between parts. Proper venting helps prevent cracks, while monitored dwell time supports stable density. Operators should check pressure sensors, mold wear, alignment, and ejection force during every production shift. These checks reveal problems before rejected parts fill a storage bin.
Manufacturers should provide pressure curves, cycle data, calibration records, and practical maintenance guidance. A machine rated for 1,000 MPa may not perform well with every powder. That assumption needs testing. Trial pressing should measure density, dimensions, surface defects, and green strength. The best equipment matches the material, part geometry, production volume, and operator skill rather than relying on maximum pressure alone.
Powder pressing begins with controlled filling. A feeder delivers metal or ceramic powder into the die cavity. Its flowability, particle size, and apparent density affect the final part. The upper and lower punches then compress the powder, often at several hundred megapascals. Pressure creates friction against the die wall, so density may vary from the surface to the core. Ejection follows carefully. Excessive speed can cause cracks, edge chipping, or springback. In practice, the pressing cycle looks simple, but small changes in powder moisture can disturb repeatability.
Tips: Measure fill depth, punch position, and ejection force on every trial. Keep a retained sample from each powder batch. It helps explain failures later.
A ±0.01 mm tolerance is possible, but it is not automatic. Tool clearance, press stiffness, temperature, and elastic recovery all matter. Many parts need sizing, calibration, or controlled sintering after pressing. A 2024 global powder metallurgy market report estimates continued growth through the decade, driven by demand for efficient material use and near-net-shape production. MPIF technical guidance also emphasizes density control and process monitoring as core quality factors. That guidance matches shop-floor experience: stable tooling often matters more than maximum tonnage. One weak assumption remains common. Operators sometimes treat the press as the whole process. It is only one link. Final inspection should verify dimensions at multiple points, not just one convenient face.
Top Powder Pressing Machine Manufacturers Worldwide
Selecting a powder pressing machine starts with force, not catalogue size. Available capacities commonly range from 5 to 500 tonnes, covering laboratory trials, small components, and industrial production. According to the Metal Powder Industries Federation’s technical guidance, compaction pressure strongly affects green density, dimensional stability, and ejection behavior. A 100-ton press may suit compact parts, but larger or taller shapes can require higher force.
Stroke and speed deserve equal attention. A longer stroke accommodates deeper dies, while controlled speed reduces uneven filling and cracking. Many production presses operate with adjustable pressing speeds, often between 5 and 50 millimeters per second. These figures vary by hydraulic or mechanical design. Faster is not always better. Powder may shift before sufficient compression develops.
Die capacity should be checked in millimeters, not broad marketing terms. Review maximum die diameter, die height, punch travel, and allowable tooling weight. Grand View Research’s Powder Metallurgy Market Size Report identifies automotive components as a major application, where repeatability and cycle time directly influence cost. Meanwhile, MarketsandMarkets reports continued growth in automated powder metallurgy equipment through the decade. Those forecasts are useful, but they can oversimplify real factory conditions. Moisture, particle size, lubrication, and operator experience still change results. A careful buyer should request test compaction data using the actual powder and die geometry.
Typical specification ranges used when comparing industrial powder pressing machine configurations worldwide.
| Machine Class | Nominal Press Force | Typical Working Stroke | Adjustable Pressing Speed | Maximum Die Capacity | Typical Part Diameter | Typical Part Height | Common Applications | Typical Drive and Control Features |
|---|---|---|---|---|---|---|---|---|
| Laboratory / Compact | 5–15 t | 50–100 mm | 1–20 mm/s | 50–100 mm | Up to 25 mm | Up to 20 mm | Material testing, prototyping, small technical ceramic and powder-metal parts | Manual or electro-hydraulic operation; force and displacement monitoring |
| Small Production | 15–50 t | 75–150 mm | 2–30 mm/s | 80–160 mm | Up to 50 mm | Up to 40 mm | Small bushings, magnets, ferrites, filters, and laboratory-scale components | Hydraulic or servo-hydraulic drive; programmable pressure and dwell time |
| Medium Production | 50–100 t | 100–200 mm | 3–40 mm/s | 120–250 mm | Up to 80 mm | Up to 60 mm | Automotive powder-metal parts, wear components, ceramic insulators, and tooling inserts | PLC or CNC control; closed-loop force, position, and multi-step pressing programs |
| Heavy Production | 100–250 t | 150–300 mm | 5–50 mm/s | 200–400 mm | Up to 140 mm | Up to 100 mm | Structural powder-metal components, large bushings, gears, ceramic bodies, and refractory parts | Servo-hydraulic or hydraulic drive; automatic powder filling and die-height adjustment options |
| Large Industrial | 250–500 t | 200–400 mm | 5–60 mm/s | 300–600 mm | Up to 250 mm | Up to 180 mm | Large powder-metal parts, industrial ceramics, refractory products, and high-density compacting | Multi-axis hydraulic or servo-hydraulic system; recipe management and automated material handling |
Note: Values are typical engineering ranges for preliminary equipment comparison. Actual capacity depends on powder characteristics, compact density, part geometry, die design, filling method, and required production cycle.
Powder pressing machine manufacturers worldwide compete through precision, durability, and process control. Leading suppliers from Europe and North America serve ceramic, technical, electrical, and metal-powder applications. Their equipment ranges from compact laboratory presses to automated production cells. Each manufacturer has a different strength. Some prioritize high-speed hydraulic systems. Others focus on servo control, modular tooling, or reliable compaction monitoring.
In practical plant evaluations, repeatability matters more than impressive brochures. Check pressure stability, die alignment, filling accuracy, and temperature control. Ask for test pieces using your actual powder blend. A machine may perform well with one formulation and struggle with another. That detail is easy to miss. Review maintenance access, spare-part availability, training, and data-recording functions. Experienced buyers also inspect noise, cycle time, and operator safety during a factory visit. No supplier is perfect; even a strong machine can need careful commissioning and process adjustment.
Tips: Compare total ownership cost, not only the purchase price. Request measured tolerances and sample-production results. Confirm local service coverage before signing. Keep a record of rejected parts during trials. That evidence supports a better decision.
The chart presents representative midpoint values from commonly reported industrial uniaxial powder-compaction pressure ranges. Actual settings vary according to powder morphology, lubricant content, tooling design, target density, and part geometry.
Comparing powder pressing machines starts with the manufacturer’s quality system. ISO 9001 certification shows controlled processes, documented inspections, and corrective actions. It does not automatically prove excellent machine performance. Ask for current certificates, audit scope, and calibration records. Check whether inspection covers the frame, hydraulic system, tooling interface, and control software. Small details matter. A stable press should hold pressure consistently during repeated cycles, not only during a demonstration.
ASTM B331 testing adds useful evidence for metal powder applications. This standard evaluates the compressive strength of sintered powder metallurgy materials. It does not certify the press itself. A responsible supplier should explain how the machine produces test specimens and how laboratories verify results. Request sample dimensions, density data, test speed, and full reports. Compare results made with your powder, because different particle sizes and binders can change behavior. One weakness remains: a polished test report may hide poor production repeatability.
Safety evaluation should include guarded moving parts, emergency stops, pressure relief, interlocks, and clear operating instructions. Ask how risks are assessed during tooling changes and maintenance. Service quality deserves equal attention. Confirm response times, spare-parts availability, remote diagnostics, training, and technician coverage in your region. A lower purchase price can become expensive when seals, sensors, or software support are delayed. No comparison is perfect. Real factory trials often reveal issues that brochures omit.
| Cookie | Duration | Description |
|---|---|---|
| AWSALB | 7 days | AWSALB is a cookie generated by the Application load balancer in the Amazon Web Services. It works slightly different from AWSELB. |
| AWSALBCORS | 7 days | This cookie is used for load balancing services provded by Amazon inorder to optimize the user experience. Amazon has updated the ALB and CLB so that customers can continue to use the CORS request with stickness. |
| cookielawinfo-checkbox-advertisement | 1 year | The cookie is set by GDPR cookie consent to record the user consent for the cookies in the category "Advertisement". |
| cookielawinfo-checkbox-analytics | 11 months | This cookie is set by GDPR Cookie Consent plugin. The cookie is used to store the user consent for the cookies in the category "Analytic / Performance". |
| cookielawinfo-checkbox-functional | 11 months | The cookie is set by GDPR cookie consent to record the user consent for the cookies in the category "Functional". |
| cookielawinfo-checkbox-necessary | 11 months | This cookie is set by GDPR Cookie Consent plugin. The cookies is used to store the user consent for the cookies in the category "Strictly Necessary". |
| cookielawinfo-checkbox-performance | 11 months | This cookie is set by GDPR Cookie Consent plugin. The cookie is used to store the user consent for the cookies in the category "Performance". |
| cookielawinfo-checkbox-preferences | 11 months | This cookie is set by GDPR Cookie Consent plugin. The cookie is used to store the user consent for the cookies in the category "Preferences." |
| elementor | never | This cookie is used by the website's WordPress theme. It allows the website owner to implement or change the website's content in real-time. |
| viewed_cookie_policy | 11 months | The cookie is set by the GDPR Cookie Consent plugin and is used to store whether or not user has consented to the use of cookies. It does not store any personal data. |
| Cookie | Duration | Description |
|---|---|---|
| CONSENT | 16 years 4 months | These cookies are set via embedded youtube-videos. They register anonymous statistical data on for example how many times the video is displayed and what settings are used for playback.No sensitive data is collected unless you log in to your google account, in that case your choices are linked with your account, for example if you click “like” on a video. |
| _ga | 2 years | This cookie is installed by Google Analytics. The cookie is used to calculate visitor, session, campaign data and keep track of site usage for the site's analytics report. The cookies store information anonymously and assign a randomly generated number to identify unique visitors. |
| _gat_gtag_UA_47200144_1 | 1 minute | This cookie is set by Google and is used to distinguish users. |
| _gid | 1 day | This cookie is installed by Google Analytics. The cookie is used to store information of how visitors use a website and helps in creating an analytics report of how the website is doing. The data collected including the number visitors, the source where they have come from, and the pages visted in an anonymous form. |
| _hjAbsoluteSessionInProgress | session | This cookie is used to count how many times a website has been visited by different visitors. This is done by assigning the visitor an ID, so the visitor does not get registered twice. |
| _hjFirstSeen | 30 minutes | This is set by Hotjar to identify a new user’s first session. It stores a true/false value, indicating whether this was the first time Hotjar saw this user. It is used by Recording filters to identify new user sessions. |
| _hjid | 1 year | This cookie is set by Hotjar. This cookie is set when the customer first lands on a page with the Hotjar script. It is used to persist the random user ID, unique to that site on the browser. This ensures that behavior in subsequent visits to the same site will be attributed to the same user ID. |
| _hjIncludedInPageviewSample | session | This cookie is used to detect whether the user navigation and interactions are included in the website’s data analytics. |
| Cookie | Duration | Description |
|---|---|---|
| IDE | 1 year 24 days | This cookie is used by Google DoubleClick and stores information about how the user uses the website and any other advertisement before visiting the website. This is used to present users with ads that are relevant to them according to the user profile. |
| NID | 6 months | This cookie is used to a profile based on user's interest and display personalized ads to the users. |
| test_cookie | 15 minutes | This cookie is set by doubleclick.net. The purpose of the cookie is to determine if the user's browser supports cookies. |
| VISITOR_INFO1_LIVE | 5 months 27 days | This cookie is set by Youtube it is used to track the information of the embedded YouTube videos on a website. |
| YSC | session | This cookies is set by Youtube and is used to track the views of embedded videos. |
| yt-remote-connected-devices | never | These cookies are set via embedded youtube-videos. |
| yt-remote-device-id | never | These cookies are set via embedded youtube-videos. |
| Cookie | Duration | Description |
|---|---|---|
| qtrans_front_language | 1 year | This cookie is set by qTranslate WordPress plugin. The cookie is used to manage the preferred language of the visitor. |