Choosing a Deep Drill Machine is not simply a matter of comparing motor power and purchase price. In a real workshop, the machine must produce accurate holes repeatedly, often through tough steel, cast iron, or engineered components. Operators notice details that catalogues may hide: vibration at the spindle, coolant reaching the cutting edge, and chips leaving the bore without clogging. Small details matter. A technically impressive model can still disappoint when its table flexes or its controls feel unclear. This guide introduces seven practical tips for evaluating drilling capacity, spindle performance, workholding, cooling, automation, safety, and long-term service support. Each point connects specifications with daily use, because a machine is judged beside the workpiece, not only on a datasheet.
Reliable selection begins with the application. Hole diameter, depth-to-diameter ratio, material hardness, tolerance, production volume, and available floor space should shape the decision. That assumption fails. More power does not automatically deliver better accuracy. A balanced spindle, rigid structure, suitable tooling, and stable coolant flow may matter more for consistent results. Experienced technicians also examine maintenance access, replacement-part availability, operator training, and manufacturer documentation. These factors influence downtime and total ownership cost long after installation. No checklist is perfect. Conditions change, and an honest evaluation may reveal that a cheaper machine suits occasional work, while a robust system earns its cost in continuous production. The following tips support careful comparison, practical testing, and informed discussions with qualified suppliers.
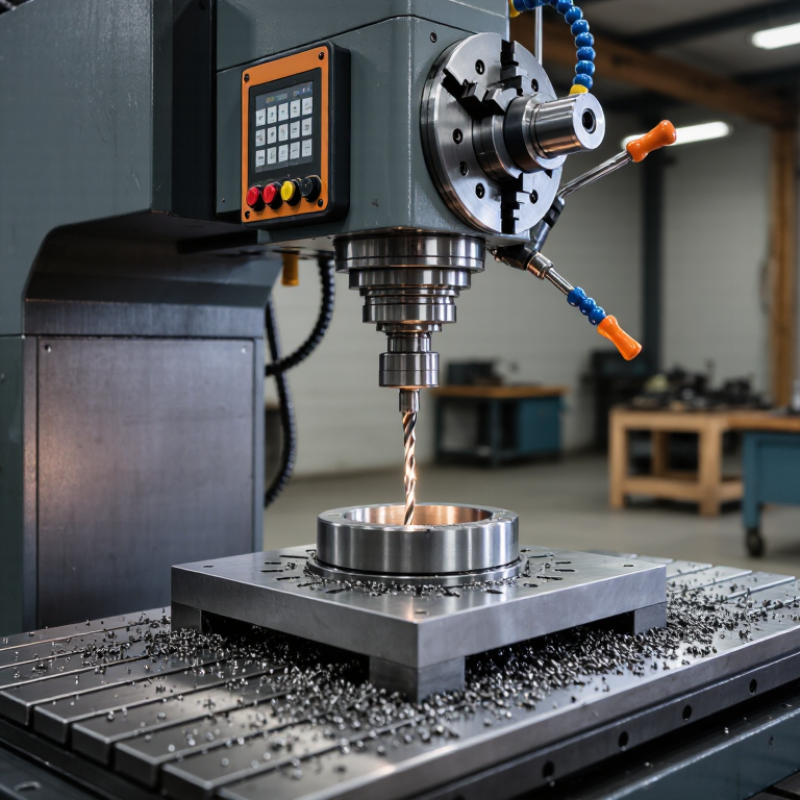
7 Tips to Choose the Best Deep Drill Machine
Deep drilling usually means a hole with a depth-to-diameter ratio of at least 10:1. For example, a 200 mm deep hole may require a 20 mm diameter. This ratio matters because long holes increase deflection, heat, chip blockage, and alignment errors. In practical machining, the opening can look accurate while the bottom drifts slightly.
Tip 1: Match the machine to the ratio, material, and required tolerance. A rigid frame, stable spindle, and controlled feed reduce vibration. Tip 2: Check the cooling and chip-removal system. Deep holes need steady coolant flow and a clear path for chips. Dry cutting may create heat quickly. Tip 3: Review real cutting data, not only catalog claims. Ask for hole-depth tests using similar steel, aluminum, or difficult alloys. Experience shows that a machine performing well at 8:1 may struggle at 15:1.
Tip 4: Examine tool guidance and spindle runout. Small alignment errors become larger down a deep hole. Tip 5: Confirm that the machine supports pecking, gun drilling, or other suitable methods. Tip 6: Measure the finished hole with reliable gauges, including straightness and diameter checks. Tip 7: Consider operator training and maintenance access. A technically strong machine can still produce poor results when setup habits are inconsistent. I would also challenge one assumption: the 10:1 ratio is a useful industry boundary, not a guarantee of quality. Material hardness, tool geometry, coolant pressure, and tolerance may demand a more capable system.
Deep drilling is commonly defined by an industry hole-depth-to-diameter ratio of at least 10:1. The chart below shows the corresponding hole depth for a 10 mm diameter hole.
As the depth-to-diameter ratio increases, chip evacuation, coolant delivery, tool rigidity, spindle accuracy, and machine stability become increasingly important. When selecting a deep drill machine, compare its rated drilling depth, coolant pressure, guide support, accuracy, and compatibility with the required hole diameter and material.
Choosing a deep drill machine starts with the hole, not the machine catalog. For diameters below 20 mm, a gun-drilling system often offers better chip control and straightness. Larger holes may require BTA or ejector drilling, especially when depth exceeds 20 times the diameter. Measure the complete depth, including breakthrough and chip clearance. A 12 mm hole, 300 mm deep, demands different rigidity than a 60 mm hole of equal depth. It is easy to underestimate that difference.
Material changes the decision. Aluminum needs sharp geometry and efficient coolant evacuation, while stainless steel requires stable feed control and strong heat removal. For hardened steel, check the Rockwell C value under ASTM E18. Materials above roughly 45 HRC may need carbide tooling, special coatings, or pre-machining. Do not rely on hardness alone. Alloy content, interrupted surfaces, and residual stress can change tool behavior. In practice, a test hole often reveals more than a specification sheet.
Machine power must match cutting torque, coolant pressure, and spindle speed. The IEA’s Energy Efficiency 2023 report estimates motor-driven systems use about 53% of global electricity, so pump and spindle efficiency deserve attention. ISO 230-2 also provides a useful framework for checking positioning accuracy. A perfect chart cannot replace inspection. Measure hole size, straightness, surface finish, and tool wear after the first batch. That first result may challenge your original choice.
Choosing a deep drill machine requires more than checking maximum drilling depth.
Real performance appears when torque, feed control, and positioning accuracy work together.
Tip 1: Check spindle torque across the working speed range. Peak torque alone can mislead. Ask for a torque curve and test a hole in the intended material.
Tip 2: Examine spindle rigidity. Hold a test bar and measure visible runout near the tool holder. Small errors become larger during deep drilling.
Tip 3: Match the spindle speed to the drill diameter and material. Excessive speed can create heat, vibration, and premature tool wear.
Tip 4: Test feed control at low, medium, and high rates. The machine should maintain steady movement without sudden stops or pressure spikes.
Tip 5: Confirm chip-breaking or pecking control. Poor timing can pack chips inside a narrow hole. That is risky for accuracy.
Tip 6: Request an ISO 230-2 positioning accuracy report. Check both repeatability and bidirectional positioning results, not only the best value.
Tip 7: Repeat the test after warm-up. Thermal drift may shift the hole position after several hours.
I have seen an accurate cold machine perform differently later.
No test is perfect. Record temperature, tool condition, workpiece setup, and measurement equipment before comparing results. A supplier should explain unusual readings clearly, rather than hiding them behind one impressive specification.
When choosing a deep drill machine, inspect coolant delivery before spindle power. In BTA deep-hole systems, pressure commonly ranges from 20 to 70 bar. That range is not a target by itself. Low pressure may leave chips packed around the cutting edge. Excessive pressure can stress seals, disturb chip control, and expose weak plumbing. Ask for measured pressure at the tool inlet, not only at the pump outlet. Pressure is lost through filters, hoses, valves, and long passages.
Match pressure with hole diameter, workpiece material, tool geometry, and drilling depth. Tough alloys often need stronger, steadier flushing. Softer materials may respond better to controlled flow than maximum pressure. Watch liters per minute too. Pressure without sufficient volume is misleading. During a trial cut, monitor the gauge, coolant temperature, chip shape, and surface finish. A stable stream should carry chips out continuously, without surging or foaming. Short interruptions matter. They can mark the bore.
Check whether the machine has separate filtration, an accessible reservoir, and alarms for low flow or pressure. Fine chips can quickly block a filter and reduce real delivery. Verify hose ratings, sealing quality, and emergency relief protection. I would also compare readings before and after the filter. The difference reveals system resistance. One imperfect assumption is common: higher bar always means faster drilling. It does not. A rigid machine with balanced coolant delivery may outperform a more powerful pump. Request a documented test using your material, diameter, depth, and tool. Generic demonstrations can hide the difficult part.
| Tip | Evaluation Dimension | Recommended Specification or Check | Why It Matters in BTA Drilling | Practical Acceptance Target |
|---|---|---|---|---|
| 1 | Coolant pressure range | Select a high-pressure coolant system adjustable from approximately 20 to 70 bar, subject to tool diameter, material, and tooling instructions. | BTA systems deliver coolant through the tool and remove chips through the drill head. Adequate pressure supports chip evacuation and stabilizes the cutting zone. | Pressure remains stable at the required flow rate during continuous drilling, without excessive pulsation. |
| 2 | Coolant flow capacity | Check the pump curve for flow at operating pressure; do not assess the pump by pressure alone. Confirm compatibility with the selected BTA head and bore diameter. | Larger holes and higher material-removal rates generally require greater coolant volume to carry chips through the return passage. | The system meets the tooling supplier’s specified flow while maintaining the required pressure at the drill head. |
| 3 | Filtration and chip separation | Use a tank and filtration arrangement designed for continuous chip loading, with accessible filters, chip collection, and differential-pressure monitoring. | BTA drilling produces chips that can restrict coolant passages, damage pumps, or cause pressure loss if they are not removed efficiently. | A visible pressure-drop indicator or alarm identifies filter loading before coolant delivery becomes inadequate. |
| 4 | Pressure and flow monitoring | Require calibrated pressure and flow gauges, plus low-pressure and low-level alarms integrated with the machine control. | A sudden pressure change may indicate a blocked tool passage, leaking seal, empty tank, or pump problem. Early detection helps prevent tool damage. | The machine can stop or feed-hold automatically when coolant pressure or flow falls below the programmed limit. |
| 5 | Coolant temperature control | Evaluate tank volume, heat-exchanger capacity, temperature sensing, and the expected heat load from spindle power and cutting time. | Temperature changes can affect coolant viscosity, tool life, dimensional stability, and the consistency of deep-hole drilling. | Coolant temperature remains within the tooling and workpiece process limits during the longest planned production cycle. |
| 6 | Seals, rotary joints, and return path | Verify that seals, rotary unions, hoses, and chip-return passages are rated for the selected pressure, coolant type, temperature, and rotational speed. | The BTA circuit depends on reliable separation between pressurized supply and chip-laden return flow. Leakage can reduce pressure and create safety risks. | No visible leakage, hose swelling, abnormal seal wear, or return-line restriction is present during a full-pressure test. |
| 7 | Coolant quality and maintenance | Use a coolant suitable for the workpiece and tooling, and define controls for concentration, pH, contamination, tramp oil, and microbial growth. | Poor coolant condition can increase corrosion, foam, odor, residue, tool wear, and filter loading, reducing drilling reliability. | Routine checks are documented, concentration is maintained within the coolant supplier’s specified range, and tank cleaning intervals are defined. |
Choosing a deep drill machine demands more than checking maximum depth. Start with chip evacuation, because packed chips can score the bore and raise cutting pressure. Compare coolant delivery, flute geometry, and chip conveyor capacity under your real material. Ask for test cuts using your diameter, depth, and production feed. A clean exit matters. I once underestimated a small coolant-flow change; the hole looked acceptable, but tool wear doubled.
Tool life should be measured per hole, not by optimistic catalog hours. Record edge wear, cycle time, surface finish, and rejected parts. A machine with automatic tool monitoring can detect abnormal load before a broken tool damages the workpiece. Automation reduces repetitive handling, yet sensors need calibration and operators need training. Never treat guarding, interlocks, emergency stops, and chip containment as optional. Watch the first production run closely.
Calculate total cost across the machine’s useful life. Include tooling, coolant, electricity, maintenance, programming, downtime, and scrap. A lower purchase price may hide expensive manual loading or frequent spindle repairs. Compare recovery time after alarms, spare-part availability, and service response in writing. Request references from shops drilling similar alloys and depths. Be skeptical of perfect demonstrations. Real floors are noisy, variable, and occasionally untidy. That is where reliability proves itself.
| Cookie | Duration | Description |
|---|---|---|
| AWSALB | 7 days | AWSALB is a cookie generated by the Application load balancer in the Amazon Web Services. It works slightly different from AWSELB. |
| AWSALBCORS | 7 days | This cookie is used for load balancing services provded by Amazon inorder to optimize the user experience. Amazon has updated the ALB and CLB so that customers can continue to use the CORS request with stickness. |
| cookielawinfo-checkbox-advertisement | 1 year | The cookie is set by GDPR cookie consent to record the user consent for the cookies in the category "Advertisement". |
| cookielawinfo-checkbox-analytics | 11 months | This cookie is set by GDPR Cookie Consent plugin. The cookie is used to store the user consent for the cookies in the category "Analytic / Performance". |
| cookielawinfo-checkbox-functional | 11 months | The cookie is set by GDPR cookie consent to record the user consent for the cookies in the category "Functional". |
| cookielawinfo-checkbox-necessary | 11 months | This cookie is set by GDPR Cookie Consent plugin. The cookies is used to store the user consent for the cookies in the category "Strictly Necessary". |
| cookielawinfo-checkbox-performance | 11 months | This cookie is set by GDPR Cookie Consent plugin. The cookie is used to store the user consent for the cookies in the category "Performance". |
| cookielawinfo-checkbox-preferences | 11 months | This cookie is set by GDPR Cookie Consent plugin. The cookie is used to store the user consent for the cookies in the category "Preferences." |
| elementor | never | This cookie is used by the website's WordPress theme. It allows the website owner to implement or change the website's content in real-time. |
| viewed_cookie_policy | 11 months | The cookie is set by the GDPR Cookie Consent plugin and is used to store whether or not user has consented to the use of cookies. It does not store any personal data. |
| Cookie | Duration | Description |
|---|---|---|
| CONSENT | 16 years 4 months | These cookies are set via embedded youtube-videos. They register anonymous statistical data on for example how many times the video is displayed and what settings are used for playback.No sensitive data is collected unless you log in to your google account, in that case your choices are linked with your account, for example if you click “like” on a video. |
| _ga | 2 years | This cookie is installed by Google Analytics. The cookie is used to calculate visitor, session, campaign data and keep track of site usage for the site's analytics report. The cookies store information anonymously and assign a randomly generated number to identify unique visitors. |
| _gat_gtag_UA_47200144_1 | 1 minute | This cookie is set by Google and is used to distinguish users. |
| _gid | 1 day | This cookie is installed by Google Analytics. The cookie is used to store information of how visitors use a website and helps in creating an analytics report of how the website is doing. The data collected including the number visitors, the source where they have come from, and the pages visted in an anonymous form. |
| _hjAbsoluteSessionInProgress | session | This cookie is used to count how many times a website has been visited by different visitors. This is done by assigning the visitor an ID, so the visitor does not get registered twice. |
| _hjFirstSeen | 30 minutes | This is set by Hotjar to identify a new user’s first session. It stores a true/false value, indicating whether this was the first time Hotjar saw this user. It is used by Recording filters to identify new user sessions. |
| _hjid | 1 year | This cookie is set by Hotjar. This cookie is set when the customer first lands on a page with the Hotjar script. It is used to persist the random user ID, unique to that site on the browser. This ensures that behavior in subsequent visits to the same site will be attributed to the same user ID. |
| _hjIncludedInPageviewSample | session | This cookie is used to detect whether the user navigation and interactions are included in the website’s data analytics. |
| Cookie | Duration | Description |
|---|---|---|
| IDE | 1 year 24 days | This cookie is used by Google DoubleClick and stores information about how the user uses the website and any other advertisement before visiting the website. This is used to present users with ads that are relevant to them according to the user profile. |
| NID | 6 months | This cookie is used to a profile based on user's interest and display personalized ads to the users. |
| test_cookie | 15 minutes | This cookie is set by doubleclick.net. The purpose of the cookie is to determine if the user's browser supports cookies. |
| VISITOR_INFO1_LIVE | 5 months 27 days | This cookie is set by Youtube it is used to track the information of the embedded YouTube videos on a website. |
| YSC | session | This cookies is set by Youtube and is used to track the views of embedded videos. |
| yt-remote-connected-devices | never | These cookies are set via embedded youtube-videos. |
| yt-remote-device-id | never | These cookies are set via embedded youtube-videos. |
| Cookie | Duration | Description |
|---|---|---|
| qtrans_front_language | 1 year | This cookie is set by qTranslate WordPress plugin. The cookie is used to manage the preferred language of the visitor. |