Choosing the best China Nozzle Cutting Machine requires more than comparing prices, power ratings, or attractive product photos. The right machine must match your material, production volume, nozzle design, and maintenance skills. A workshop cutting stainless steel sheets may need different performance from a factory processing carbon steel every day. Small details matter. Nozzle diameter, centering accuracy, cooling stability, and replacement-part availability can directly affect cut quality.
Laser-cutting specialist John Powell has stated, “The laser beam is only as good as the system that delivers it.” This principle applies closely to every Nozzle Cutting Machine. A powerful laser cannot compensate for poor nozzle alignment, unstable gas flow, or careless calibration. During practical testing, operators should inspect edge smoothness, piercing time, slag buildup, and beam consistency across repeated jobs. Results should be recorded, not guessed.
There is no flawless machine for every buyer. Some Chinese manufacturers offer excellent automation but limited technical support in overseas markets. Others provide reliable cutting performance, yet their software may feel less refined. That difference can become expensive after installation. Buyers should examine factory experience, certification records, warranty terms, training quality, and real customer feedback. A factory visit or live cutting test is even better.
This guide compares leading options through an experience-based and technical lens. It also recognizes an uncomfortable point: the cheapest machine may not be the most economical choice. Long-term reliability, service response, and nozzle consistency often matter more than the first quotation.
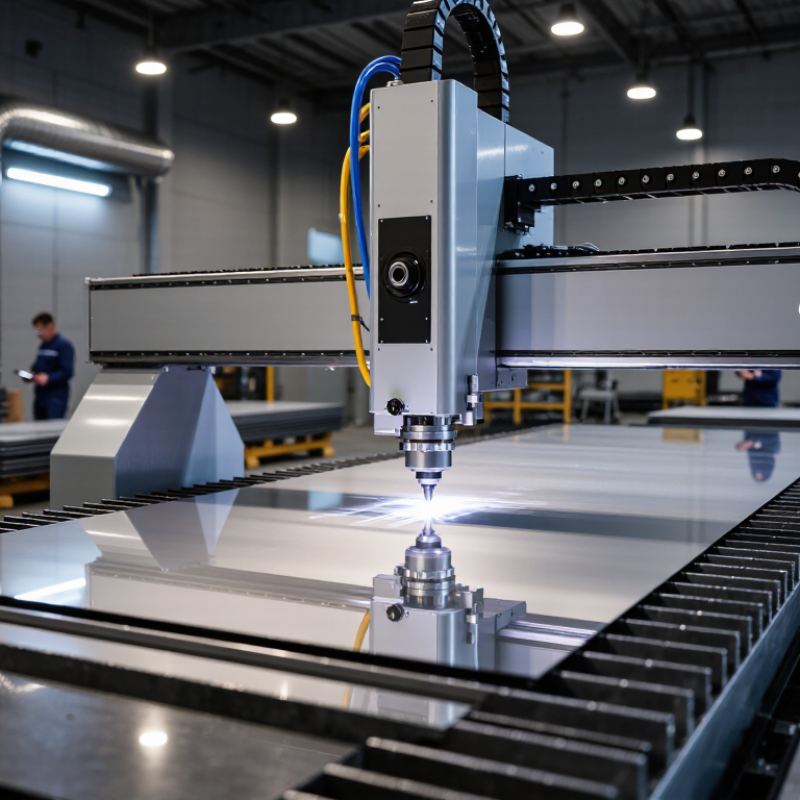
A China nozzle cutting machine is a computer-controlled system designed to produce precise nozzles from metal or other suitable materials. In many workshops, it uses laser, plasma, or mechanical cutting technology. The correct process depends on material thickness, nozzle geometry, and required tolerance.
The machine usually combines a cutting head, motion table, control software, and fixture. The fixture holds each workpiece firmly during cutting. This matters because even slight movement can create an uneven opening. Operators commonly adjust cutting speed, power, gas pressure, and focal position. Small changes can affect edge quality.
A reliable evaluation should begin with sample cutting, not promises. Ask for measured results, repeatability records, and compatible material data. Check whether the control system supports the shapes your production actually needs. Maintenance access also matters. Dust, heat, and metal particles can reduce performance over time.
Not every machine is equal.
In practical testing, inspect the finished nozzle under magnification. Look for burrs, taper, cracks, or heat discoloration. A clean edge may improve airflow and service life, but cutting quality is only one factor. Tool stability, operator training, spare parts, and safety controls also influence the final result. The term “China nozzle cutting machine” describes an origin and machine category, not a guaranteed level of quality. A careful buyer should verify each technical claim. Mistakes happen, especially when specifications are copied without testing.
Which Is the Best China Nozzle Cutting Machine?
How Do Nozzle Cutting Machines Work?
A nozzle cutting machine converts a digital drawing into controlled tool movement. The operator loads the nozzle blank and secures it inside a chuck or fixture. A controller then reads the programmed cutting path. The spindle or cutting head follows that path around the workpiece. Depending on the material, the machine may use a laser, plasma arc, or mechanical cutter.
Accurate cutting depends on several coordinated actions. The fixture keeps the nozzle stable while the head maintains a consistent distance. Sensors may check height, edge position, and material location. Cutting speed, power, gas flow, and feed rate are adjusted for the material thickness. A stainless steel nozzle needs different settings from an aluminum one. Small errors can create rough edges or an uneven outlet.
The process is not completely automatic. Operators inspect the first piece with calipers, gauges, or visual checks. They may adjust the tool path after finding burrs or heat marks. Real production conditions are less perfect than machine manuals suggest. Dust, vibration, and worn tools can slowly reduce accuracy. That detail is easy to miss. Regular nozzle cleaning and calibration help maintain stable results. A reliable machine should also record settings, support repeatable programs, and allow practical maintenance without excessive downtime.
| Machine Type | Working Principle | Typical Materials | Typical Cutting Thickness | Main Cutting Gas or Medium | Typical Strengths | Important Selection Factors |
|---|---|---|---|---|---|---|
| Fiber Laser Cutting Machine | A fiber laser generates a concentrated light beam. The beam is focused through a cutting head, while an assist gas removes molten material through the nozzle. | Mild steel, stainless steel, aluminum, brass, copper, and galvanized sheet | Commonly used for thin and medium metal sheets; the practical range depends on laser power, material type, and required edge quality. | Oxygen, nitrogen, or compressed air | High precision, narrow kerf, fast processing of sheet metal, and good automation potential | Laser power, cutting-head quality, autofocus control, machine rigidity, assist-gas pressure, and nozzle alignment |
| CO₂ Laser Cutting Machine | A gas laser uses an electrically excited carbon-dioxide mixture to produce an infrared beam, which is focused onto the workpiece and supported by an assist gas. | Carbon steel, stainless steel, acrylic, wood, plastics, textiles, and other nonmetal materials, depending on configuration | Suitable for a broad range of thin and medium materials; the maximum thickness varies significantly with power and material. | Oxygen, nitrogen, air, or another application-specific assist gas | Flexible material compatibility, especially for some nonmetal applications | Operating cost, optical-path maintenance, material compatibility, cooling system, and extraction requirements |
| Plasma Cutting Machine | An electric arc ionizes compressed gas into plasma. The high-temperature plasma melts the metal, and the fast gas stream ejects the molten material through the cut. | Carbon steel, stainless steel, aluminum, and other electrically conductive metals | Often selected for medium to thick conductive metal; capacity depends on the plasma power source and torch design. | Compressed air, oxygen, nitrogen, or argon-hydrogen mixtures | High cutting speed on conductive metals and lower entry cost than many laser systems | Required edge quality, consumable life, torch height control, electrical capacity, and fume extraction |
| Oxy-Fuel Cutting Machine | A fuel gas preheats the steel, then a jet of oxygen reacts with the hot metal and removes the resulting iron oxide from the cut zone. | Primarily carbon steel and low-alloy steel; not generally suitable for stainless steel or aluminum | Well suited to thick carbon-steel plate, with capacity determined by torch, gas pressure, and machine configuration. | Oxygen combined with acetylene, propane, or another fuel gas | Effective for thick steel, relatively simple equipment, and suitability for large plate processing | Heat-affected zone, preheating time, gas safety, plate thickness, and required dimensional accuracy |
| Waterjet Cutting Machine | A high-pressure water stream, sometimes mixed with abrasive particles, erodes the material without creating a conventional heat-affected zone. | Metal, stone, glass, ceramics, composites, rubber, and many heat-sensitive materials | Can process thin to very thick materials; the actual limit depends on pump pressure, abrasive flow, and material properties. | High-pressure water; abrasive garnet is commonly used for hard materials | Cold cutting, low thermal distortion, and broad material compatibility | Water and abrasive consumption, pump maintenance, cutting speed, drainage, and operating cost |
| Nozzle Function | The nozzle directs and shapes the assist-gas stream around the laser beam or plasma arc. It helps remove molten material and influences cut stability. | Relevant to laser and plasma cutting systems | Not applicable as a thickness category; the correct nozzle depends on the cutting process and material thickness. | Oxygen, nitrogen, compressed air, or process-specific plasma gas | Stable gas flow, reduced spatter, improved edge quality, and more consistent piercing | Nozzle diameter, nozzle-to-workpiece distance, concentricity, cleanliness, wear, and gas pressure |
| Single-Layer Laser Nozzle | Uses one internal gas path to deliver the assist gas around the focused laser beam. | Commonly used for oxygen or nitrogen cutting when the process requires a straightforward gas flow path | Selected according to material, gas type, power level, and cutting parameters rather than thickness alone. | Oxygen, nitrogen, or compressed air | Simple structure, easy maintenance, and suitable gas-flow performance for many standard applications | Correct orifice size, gas-flow uniformity, beam-nozzle centering, and compatibility with the cutting head |
| Double-Layer Laser Nozzle | Uses separate inner and outer passages to support different gas-flow arrangements and process requirements. | Metal sheets and plates processed with laser cutting systems | Application-dependent; nozzle selection should follow the material, assist gas, focal position, and cutting parameters. | Oxygen, nitrogen, or compressed air, depending on the nozzle design | Can provide stable gas delivery for specific cutting and piercing conditions | Internal passage design, sealing condition, nozzle height, cleanliness, and correct gas-pressure setting |
| Best Selection Criteria | The best machine is determined by matching the cutting method to the material, thickness, tolerance, production volume, and operating environment. | Material type, reflectivity, electrical conductivity, heat sensitivity, and surface condition | Choose a machine with a rated capacity above the normal production thickness to maintain process stability. | Gas availability, purity, pressure, flow rate, and operating cost | For many sheet-metal applications, a properly configured fiber laser is a strong general-purpose option. | Compare accuracy, throughput, serviceability, consumable cost, safety systems, software, extraction, and total cost of ownership. |
| Nozzle Maintenance | Routine inspection keeps the nozzle orifice clean and concentric, allowing the assist gas and cutting beam or arc to remain properly aligned. | All laser and plasma cutting applications | Maintenance frequency depends on material, piercing frequency, spatter, and operating conditions. | The gas specified by the cutting process and material recipe | More stable piercing, fewer alarms, improved cut quality, and longer consumable life | Clean the tip, check for deformation, verify centering, inspect ceramic or insulation parts, and replace damaged nozzles. |
Which Is the Best China Nozzle Cutting Machine?
Which Features Define a High-Quality Cutting Machine?
A high-quality nozzle cutting machine starts with stable cutting performance. The nozzle should hold a precise, centered orifice during repeated use. Even a small opening error can create uneven edges, excess heat, or poor material separation. Check the nozzle material, heat resistance, and machining tolerance before comparing prices.
Practical testing matters. Ask for sample cuts on your actual material and thickness. Examine the edge under bright light. Look for burrs, taper, slag, or visible width changes. A reliable machine should control speed, gas flow, power, and cutting height with steady adjustments. Its control system should also record settings, making repeat production easier.
Maintenance is easy to underestimate. I once focused too heavily on cutting speed and ignored nozzle cleaning. That decision caused inconsistent results. The better choice included simple access, clear replacement steps, and readily available technical guidance. Check whether the machine supports automatic height sensing, overload protection, and accurate positioning. Service response also matters, especially when production stops unexpectedly.
Some details still require judgment. A heavier frame may improve stability, but it can increase installation demands. Higher power may expand capacity, yet it can raise operating costs. Review test data, tolerance reports, operator feedback, and warranty terms together. One impressive demonstration is not enough.
Which Is the Best China Nozzle Cutting Machine?
How to Compare China Nozzle Cutting Machine Manufacturers?
The best manufacturer is not always the lowest-priced supplier. Start by checking nozzle material compatibility, cutting accuracy, gas-channel design, and repeatability. ISO 9013:2017 classifies thermal-cut quality through dimensional accuracy, angularity, and surface roughness. Ask each supplier for measured results, not promotional claims. Request samples cut from copper, brass, or stainless steel. Inspect the orifice under magnification. Small burrs can disturb gas flow and shorten service life.
Market data also supports a careful evaluation. Grand View Research projects strong growth in the global laser cutting machine market through 2030, driven by automation and precision manufacturing. Deloitte’s 2024 Smart Manufacturing Survey reported that 86% of manufacturers view smart production as important for future competitiveness. Therefore, compare software integration, sensor feedback, data export, and remote diagnostics. A machine without useful production records may become expensive later. It happens.
During supplier audits, examine calibration certificates, incoming-material checks, operator training, and spare-part availability. Ask for the actual tolerance range across several production batches. One perfect sample proves very little. Review warranty terms, response times, installation support, and replacement-nozzle lead times. A factory tour helps, but it is not evidence by itself. My own caution is simple: polished presentations can hide weak process control. Independent testing remains the safer comparison method.
How to compare China nozzle cutting machine manufacturers using a practical procurement-weighting model.
The percentages represent recommended evaluation weights for comparing manufacturers. Cutting quality, machine reliability, service support, total cost of ownership, safety compliance, delivery capability, and customization should be assessed together rather than judged by price alone. Use the same scoring system and request documented evidence for every supplier.
Choosing the best China nozzle cutting machine depends on your material, workload, and required accuracy. A small fabrication shop may need a compact CNC unit for occasional stainless steel nozzles. A busy production line may require automatic feeding, stable cooling, and faster cycle times. The cheapest machine is not always the best fit.
In practical workshop checks, I examine cut consistency at the nozzle opening first. A clean edge reduces later polishing and improves assembly accuracy. I also inspect the control system, cutting head movement, and replacement-part access. Ask for test samples using your actual metal thickness. Photos can hide rough edges. Test data is stronger evidence.
Material changes everything. Thin stainless steel may favor precision laser cutting, while thicker steel may need a different cutting method. Check the machine’s working range, positioning tolerance, power requirements, and dust-control design. Operator training also matters. A sophisticated machine can underperform when setup instructions are unclear. I once focused too heavily on cutting speed and overlooked maintenance time. That mistake increased production delays. Service response, warranty terms, and available technical support deserve equal attention. Leave room for future orders, but avoid paying for features your workshop will never use.
| Cookie | Duration | Description |
|---|---|---|
| AWSALB | 7 days | AWSALB is a cookie generated by the Application load balancer in the Amazon Web Services. It works slightly different from AWSELB. |
| AWSALBCORS | 7 days | This cookie is used for load balancing services provded by Amazon inorder to optimize the user experience. Amazon has updated the ALB and CLB so that customers can continue to use the CORS request with stickness. |
| cookielawinfo-checkbox-advertisement | 1 year | The cookie is set by GDPR cookie consent to record the user consent for the cookies in the category "Advertisement". |
| cookielawinfo-checkbox-analytics | 11 months | This cookie is set by GDPR Cookie Consent plugin. The cookie is used to store the user consent for the cookies in the category "Analytic / Performance". |
| cookielawinfo-checkbox-functional | 11 months | The cookie is set by GDPR cookie consent to record the user consent for the cookies in the category "Functional". |
| cookielawinfo-checkbox-necessary | 11 months | This cookie is set by GDPR Cookie Consent plugin. The cookies is used to store the user consent for the cookies in the category "Strictly Necessary". |
| cookielawinfo-checkbox-performance | 11 months | This cookie is set by GDPR Cookie Consent plugin. The cookie is used to store the user consent for the cookies in the category "Performance". |
| cookielawinfo-checkbox-preferences | 11 months | This cookie is set by GDPR Cookie Consent plugin. The cookie is used to store the user consent for the cookies in the category "Preferences." |
| elementor | never | This cookie is used by the website's WordPress theme. It allows the website owner to implement or change the website's content in real-time. |
| viewed_cookie_policy | 11 months | The cookie is set by the GDPR Cookie Consent plugin and is used to store whether or not user has consented to the use of cookies. It does not store any personal data. |
| Cookie | Duration | Description |
|---|---|---|
| CONSENT | 16 years 4 months | These cookies are set via embedded youtube-videos. They register anonymous statistical data on for example how many times the video is displayed and what settings are used for playback.No sensitive data is collected unless you log in to your google account, in that case your choices are linked with your account, for example if you click “like” on a video. |
| _ga | 2 years | This cookie is installed by Google Analytics. The cookie is used to calculate visitor, session, campaign data and keep track of site usage for the site's analytics report. The cookies store information anonymously and assign a randomly generated number to identify unique visitors. |
| _gat_gtag_UA_47200144_1 | 1 minute | This cookie is set by Google and is used to distinguish users. |
| _gid | 1 day | This cookie is installed by Google Analytics. The cookie is used to store information of how visitors use a website and helps in creating an analytics report of how the website is doing. The data collected including the number visitors, the source where they have come from, and the pages visted in an anonymous form. |
| _hjAbsoluteSessionInProgress | session | This cookie is used to count how many times a website has been visited by different visitors. This is done by assigning the visitor an ID, so the visitor does not get registered twice. |
| _hjFirstSeen | 30 minutes | This is set by Hotjar to identify a new user’s first session. It stores a true/false value, indicating whether this was the first time Hotjar saw this user. It is used by Recording filters to identify new user sessions. |
| _hjid | 1 year | This cookie is set by Hotjar. This cookie is set when the customer first lands on a page with the Hotjar script. It is used to persist the random user ID, unique to that site on the browser. This ensures that behavior in subsequent visits to the same site will be attributed to the same user ID. |
| _hjIncludedInPageviewSample | session | This cookie is used to detect whether the user navigation and interactions are included in the website’s data analytics. |
| Cookie | Duration | Description |
|---|---|---|
| IDE | 1 year 24 days | This cookie is used by Google DoubleClick and stores information about how the user uses the website and any other advertisement before visiting the website. This is used to present users with ads that are relevant to them according to the user profile. |
| NID | 6 months | This cookie is used to a profile based on user's interest and display personalized ads to the users. |
| test_cookie | 15 minutes | This cookie is set by doubleclick.net. The purpose of the cookie is to determine if the user's browser supports cookies. |
| VISITOR_INFO1_LIVE | 5 months 27 days | This cookie is set by Youtube it is used to track the information of the embedded YouTube videos on a website. |
| YSC | session | This cookies is set by Youtube and is used to track the views of embedded videos. |
| yt-remote-connected-devices | never | These cookies are set via embedded youtube-videos. |
| yt-remote-device-id | never | These cookies are set via embedded youtube-videos. |
| Cookie | Duration | Description |
|---|---|---|
| qtrans_front_language | 1 year | This cookie is set by qTranslate WordPress plugin. The cookie is used to manage the preferred language of the visitor. |