Choosing a Blow Maker is not merely a machinery decision. It shapes product quality, production speed, energy use, and long-term operating costs.
A suitable Blow Maker can produce consistent containers with accurate wall thickness and cleaner surface finishes. It can also reduce material waste when settings are carefully controlled. Dr. Michael Thielen, a recognized blow-molding author and technical educator, has emphasized this practical principle: “The right machine must match the product, material, and production volume.” That idea deserves attention. A high-output machine may appear attractive, yet it can become inefficient for a small factory with limited orders. Bigger is not always better.
Experience on the production floor reveals details that brochures often overlook. Operators need clear controls, accessible maintenance points, and reliable technical support. A machine that stops beside a cooling line can delay an entire shift. Small failures become expensive quickly. A thoughtful Blow Maker selection should consider mold compatibility, resin requirements, cycle time, safety features, and future capacity. Energy consumption matters too, especially when the machine runs daily.
There is no perfect choice.
Even experienced buyers can misjudge demand or underestimate training needs. Reviewing sample products, testing materials, and comparing documented performance can prevent costly assumptions. Businesses should also verify supplier credentials, service response times, replacement-part availability, and applicable safety standards. The best Blow Maker is not simply the fastest option. It is the one that delivers dependable results, supports responsible production, and fits the company’s real operating conditions.
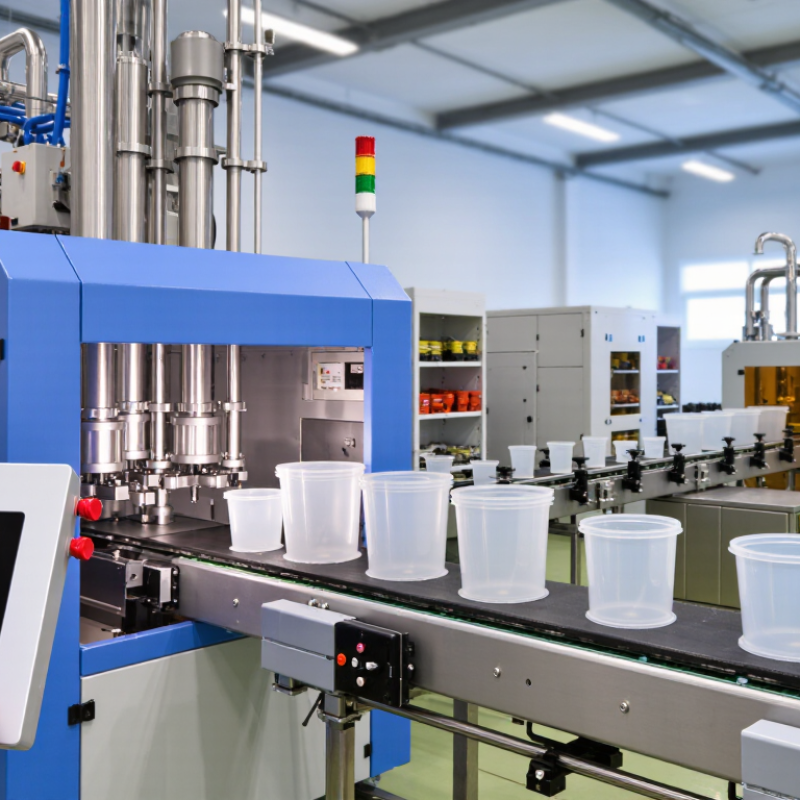
A blow maker usually means a blow molding machine. It forms hollow plastic products, such as bottles, containers, and industrial tanks.
The process begins with plastic pellets. Heat turns them into a soft tube called a parison. A mold then closes around it. Compressed air expands the parison against the mold walls. Cooling hardens the shape. The machine opens, and operators remove the finished part.
Different machines suit different production needs. Extrusion blow molding handles many containers efficiently. Injection blow molding offers precise neck finishes. Stretch blow molding improves strength and clarity for selected packaging.
Grand View Research estimates the global blow molding machine market will grow at about 4.8% annually from 2024 to 2030. That growth reflects demand for lightweight packaging and automated production. However, buying capacity alone is not enough. Energy use, mold changes, scrap rates, and maintenance access also affect real costs. The first setup is rarely perfect.
Tips:
Test the material, mold, and air pressure together. Track cycle time, cooling time, and rejected units. The Plastics Industry Association reports that energy efficiency remains a major manufacturing priority. Start with a small production trial. Check wall thickness at several points, especially near corners and the base. A small air leak can quietly reduce output. Operators should also review ventilation, guarding, and training before full operation. A machine may look efficient on paper, yet perform differently on a busy factory floor.
A blow maker can produce many hollow plastic products with consistent wall thickness and repeatable shapes. Common examples include water bottles, detergent containers, cooking oil bottles, and cosmetic packaging. The process forms a heated plastic tube inside a mold, then expands it with controlled air pressure. This creates lightweight containers with accurate necks, handles, and openings.
In practical production, a blow maker can also manufacture jerry cans, storage tanks, fuel containers, and wide-mouth household vessels. Some machines produce technical parts, such as air ducts, protective covers, and small industrial housings. Product size depends on the machine’s clamping force, mold design, material choice, and extrusion capacity. A small unit may handle bottles, while a larger system can form containers measuring several meters.
Details matter. A container may look simple, yet its corners, grip area, and base need careful testing. Uneven cooling can cause distortion or weak spots. I have seen projects focus too heavily on output speed and overlook mold maintenance. That mistake becomes expensive. Product testing should check leakage, drop resistance, weight variation, and dimensional accuracy. Food or personal-care packaging also requires suitable materials and controlled production conditions. Not every blow maker fits every product. The right choice depends on shape, volume, resin behavior, and required quality standards.
A blow maker can turn plastic containers from a design file into consistent, usable products. In a small packaging workshop, operators may produce hundreds of bottles during one shift. Automated forming reduces repetitive manual work and keeps production speed more stable. That matters when customers expect regular deliveries.
The machine also supports better product consistency. Controlled temperature, air pressure, and cycle timing can help maintain wall thickness and container shape. Less variation can reduce rejected units and material waste. However, these benefits depend on accurate settings and trained operators. A poorly adjusted mold can create thin corners, uneven surfaces, or weak necks. It is not a magic solution.
A blow maker can improve flexibility, too. Businesses may switch between container sizes by changing molds and production parameters. This can support seasonal packaging or smaller product runs without rebuilding the entire process. Modern equipment may also record operating data, helping technicians identify pressure changes or heating problems early. Maintenance remains essential. Dust, worn seals, and blocked air lines can quietly reduce performance. Energy use deserves attention as well, because an efficient machine may lower long-term operating costs, but the purchase price is only one part of the decision. Businesses should compare output, service access, training needs, safety features, and expected downtime before investing.
Choosing the right blow maker starts with your product, not the machine’s advertised speed. Define the container shape, volume, wall thickness, and material before comparing equipment. A small bottle may need different forming control than a wide chemical container. Your target output also matters. Calculate hourly demand, shift length, and expected future growth. Buying excessive capacity can increase energy costs and maintenance pressure.
Inspect the machine’s forming accuracy, temperature control, mold compatibility, and changeover time. During production trials, measure bottle weight, thickness distribution, leakage rates, and rejected units. A fast cycle means little if quality varies between the first and last cavity. Ask for service response times, spare-part availability, operator training, and documented safety procedures. Local technical support can prevent a minor sensor fault from stopping production for days. Energy monitoring is useful too, although actual consumption may differ from supplier estimates.
Tips: Test your own material and mold before purchase. Check samples under normal production conditions, not only in a showroom. Speak with operators who use similar equipment. Their practical comments may reveal noise, cleaning difficulties, or awkward access points. Do not choose only by price. I have seen low initial costs become expensive after repeated adjustments. Still, a premium machine is not automatically the best choice. Review the full operating cost, maintenance records, warranty terms, and measurable product results before deciding.
| Blow-Molding Type | Typical Container Range | Common Materials | Typical Applications | Main Advantages | Key Limitations | Best Business Fit |
|---|---|---|---|---|---|---|
| Extrusion Blow Molding | Approximately 50 ml to more than 200 L, depending on machine configuration | HDPE, LDPE, PP, PVC, PETG and selected engineering plastics | Bottles, jerry cans, industrial containers, drums, automotive ducts and technical parts | Flexible tooling, suitable for complex shapes, economical for medium-to-large containers and multilayer structures | Higher material scrap than some other processes; wall-thickness control may require advanced programming | Businesses producing varied container designs or durable industrial packaging |
| Injection Blow Molding | Generally about 5 ml to 2 L for precision containers | PE, PP, PET and selected specialty polymers | Pharmaceutical bottles, cosmetic containers, small food packages and laboratory products | Accurate neck finishes, consistent dimensions, good appearance and minimal or no flash | Higher tooling cost and less flexibility for very large containers; usually requires precise molds | Businesses prioritizing dimensional accuracy, clean appearance and repeatable small-container production |
| Injection Stretch Blow Molding | Commonly about 100 ml to 3 L, with larger sizes possible on specialized systems | PET, PEN and selected copolyesters | Water bottles, carbonated beverage bottles, edible-oil containers and personal-care packaging | Strong, lightweight containers with good clarity and efficient material distribution through biaxial stretching | Requires preform production or preforms as an input; process settings are sensitive to temperature and stretch conditions | High-volume PET packaging operations where lightweighting and transparency are important |
| Two-Stage PET Blow Molding | Typically about 200 ml to 20 L, depending on the preform and machine design | PET and selected recycled-PET blends, subject to material and application requirements | Beverage bottles, household products, edible-oil packaging and specialty clear containers | High output, strong lightweight bottles and the ability to separate preform manufacturing from final blowing | Requires preform inventory and controlled heating; unsuitable for many non-PET applications | Businesses with stable demand for clear PET containers and scalable production volumes |
| Decision Factor | What to Evaluate | Recommended Direction | Business Impact |
|---|---|---|---|
| Product Size and Shape | Container volume, height, neck finish, handle design, wall thickness and shape complexity | Match the clamping force, mold dimensions, parison or preform capacity and machine stroke to the product | Reduces mold-fit problems, rejects and limitations when introducing new products |
| Required Output | Target units per hour, number of cavities, operating schedule and expected future demand | Choose a machine with practical capacity above the current target instead of relying only on maximum rated output | Supports delivery commitments while allowing for maintenance, changeovers and demand growth |
| Material Compatibility | Resin type, melt temperature, recycled-content requirements, additives and barrier-layer needs | Confirm screw, barrel, heating system and material-drying requirements before purchase | Improves product quality and helps prevent material degradation or unstable processing |
| Energy Consumption | Heating zones, hydraulic or servo systems, compressor demand, cooling load and standby consumption | Compare measured energy use per 1,000 containers under the same product and operating conditions | Affects operating cost, carbon footprint and long-term return on investment |
| Automation and Control | Recipe storage, process monitoring, automatic rejection, mold changeover and data access | Select controls that provide repeatable settings and clear alarms for the operator skill level available | Reduces setup time, labor dependency and variation between production batches |
| Quality Requirements | Weight variation, wall-thickness distribution, leak rate, visual defects and dimensional tolerances | Request sample production and inspect containers using the same resin, mold and target cycle | Provides evidence that the machine can meet commercial specifications before installation |
| Maintenance and Support | Availability of wear parts, service response, technical training, documentation and local expertise | Evaluate total ownership cost and planned maintenance requirements, not only purchase price | Improves uptime and reduces the financial impact of unexpected stoppages |
| Factory Space and Utilities | Machine footprint, mold area, ceiling height, electrical supply, compressed air, water and ventilation | Confirm the complete installation layout and utility load before finalizing the machine | Avoids installation delays, unexpected infrastructure costs and restricted production flow |
Note: Capacity and container-size ranges are typical industry ranges and vary according to machine configuration, mold design, resin characteristics, cavity count and operating conditions. Final selection should be confirmed through a production trial and a complete utility and cost assessment.
A blow maker can support steady production, but its purchase price is only one part of the investment. The final cost depends on output volume, container size, material type, automation level, and mold design. A machine for thick containers often needs stronger heating and higher air pressure. That difference appears in energy bills.
Maintenance begins with operating conditions. Dust, moisture, unstable compressed air, and poor cooling can shorten component life. Filters, heaters, valves, seals, and mold surfaces need regular inspection. In my experience, neglected air filtration causes small faults before major failures appear. A pressure gauge may drift, while a worn seal quietly increases air consumption. These details are easy to miss.
A reliable cost estimate should include installation, operator training, utilities, preventive maintenance, and emergency repairs. Ask about service intervals and typical replacement times, not only the equipment price. During a trial run, record cycle time, reject rate, air pressure, and energy consumption. These measurements provide stronger evidence than a polished forecast. Still, no estimate is perfect. Production changes. A lower upfront cost can become expensive when access is difficult or replacement parts arrive slowly. Plan around real working conditions, including cleaning time, technician availability, and occasional downtime.
A blow molding machine can improve production consistency and reduce unit costs at higher volumes. The main cost and maintenance drivers are machine size, output capacity, tooling complexity, energy demand, and operating hours.
Indicative industry planning ranges for new blow molding equipment. Actual costs vary by machine configuration, automation level, mold design, local labor, utilities, and service requirements.
| Cookie | Duration | Description |
|---|---|---|
| AWSALB | 7 days | AWSALB is a cookie generated by the Application load balancer in the Amazon Web Services. It works slightly different from AWSELB. |
| AWSALBCORS | 7 days | This cookie is used for load balancing services provded by Amazon inorder to optimize the user experience. Amazon has updated the ALB and CLB so that customers can continue to use the CORS request with stickness. |
| cookielawinfo-checkbox-advertisement | 1 year | The cookie is set by GDPR cookie consent to record the user consent for the cookies in the category "Advertisement". |
| cookielawinfo-checkbox-analytics | 11 months | This cookie is set by GDPR Cookie Consent plugin. The cookie is used to store the user consent for the cookies in the category "Analytic / Performance". |
| cookielawinfo-checkbox-functional | 11 months | The cookie is set by GDPR cookie consent to record the user consent for the cookies in the category "Functional". |
| cookielawinfo-checkbox-necessary | 11 months | This cookie is set by GDPR Cookie Consent plugin. The cookies is used to store the user consent for the cookies in the category "Strictly Necessary". |
| cookielawinfo-checkbox-performance | 11 months | This cookie is set by GDPR Cookie Consent plugin. The cookie is used to store the user consent for the cookies in the category "Performance". |
| cookielawinfo-checkbox-preferences | 11 months | This cookie is set by GDPR Cookie Consent plugin. The cookie is used to store the user consent for the cookies in the category "Preferences." |
| elementor | never | This cookie is used by the website's WordPress theme. It allows the website owner to implement or change the website's content in real-time. |
| viewed_cookie_policy | 11 months | The cookie is set by the GDPR Cookie Consent plugin and is used to store whether or not user has consented to the use of cookies. It does not store any personal data. |
| Cookie | Duration | Description |
|---|---|---|
| CONSENT | 16 years 4 months | These cookies are set via embedded youtube-videos. They register anonymous statistical data on for example how many times the video is displayed and what settings are used for playback.No sensitive data is collected unless you log in to your google account, in that case your choices are linked with your account, for example if you click “like” on a video. |
| _ga | 2 years | This cookie is installed by Google Analytics. The cookie is used to calculate visitor, session, campaign data and keep track of site usage for the site's analytics report. The cookies store information anonymously and assign a randomly generated number to identify unique visitors. |
| _gat_gtag_UA_47200144_1 | 1 minute | This cookie is set by Google and is used to distinguish users. |
| _gid | 1 day | This cookie is installed by Google Analytics. The cookie is used to store information of how visitors use a website and helps in creating an analytics report of how the website is doing. The data collected including the number visitors, the source where they have come from, and the pages visted in an anonymous form. |
| _hjAbsoluteSessionInProgress | session | This cookie is used to count how many times a website has been visited by different visitors. This is done by assigning the visitor an ID, so the visitor does not get registered twice. |
| _hjFirstSeen | 30 minutes | This is set by Hotjar to identify a new user’s first session. It stores a true/false value, indicating whether this was the first time Hotjar saw this user. It is used by Recording filters to identify new user sessions. |
| _hjid | 1 year | This cookie is set by Hotjar. This cookie is set when the customer first lands on a page with the Hotjar script. It is used to persist the random user ID, unique to that site on the browser. This ensures that behavior in subsequent visits to the same site will be attributed to the same user ID. |
| _hjIncludedInPageviewSample | session | This cookie is used to detect whether the user navigation and interactions are included in the website’s data analytics. |
| Cookie | Duration | Description |
|---|---|---|
| IDE | 1 year 24 days | This cookie is used by Google DoubleClick and stores information about how the user uses the website and any other advertisement before visiting the website. This is used to present users with ads that are relevant to them according to the user profile. |
| NID | 6 months | This cookie is used to a profile based on user's interest and display personalized ads to the users. |
| test_cookie | 15 minutes | This cookie is set by doubleclick.net. The purpose of the cookie is to determine if the user's browser supports cookies. |
| VISITOR_INFO1_LIVE | 5 months 27 days | This cookie is set by Youtube it is used to track the information of the embedded YouTube videos on a website. |
| YSC | session | This cookies is set by Youtube and is used to track the views of embedded videos. |
| yt-remote-connected-devices | never | These cookies are set via embedded youtube-videos. |
| yt-remote-device-id | never | These cookies are set via embedded youtube-videos. |
| Cookie | Duration | Description |
|---|---|---|
| qtrans_front_language | 1 year | This cookie is set by qTranslate WordPress plugin. The cookie is used to manage the preferred language of the visitor. |